Ubufatanye
UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
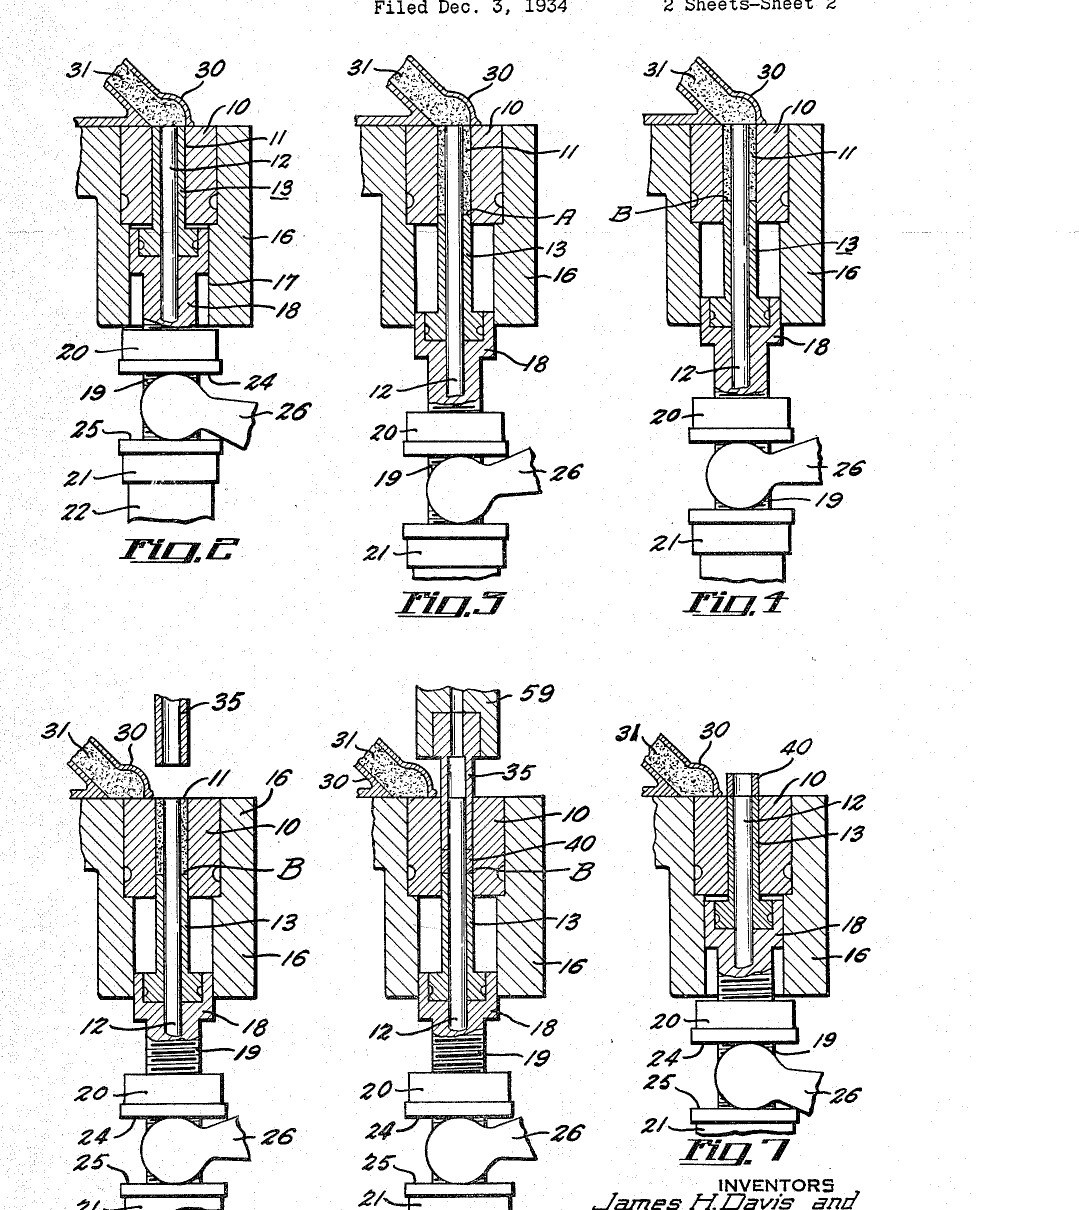

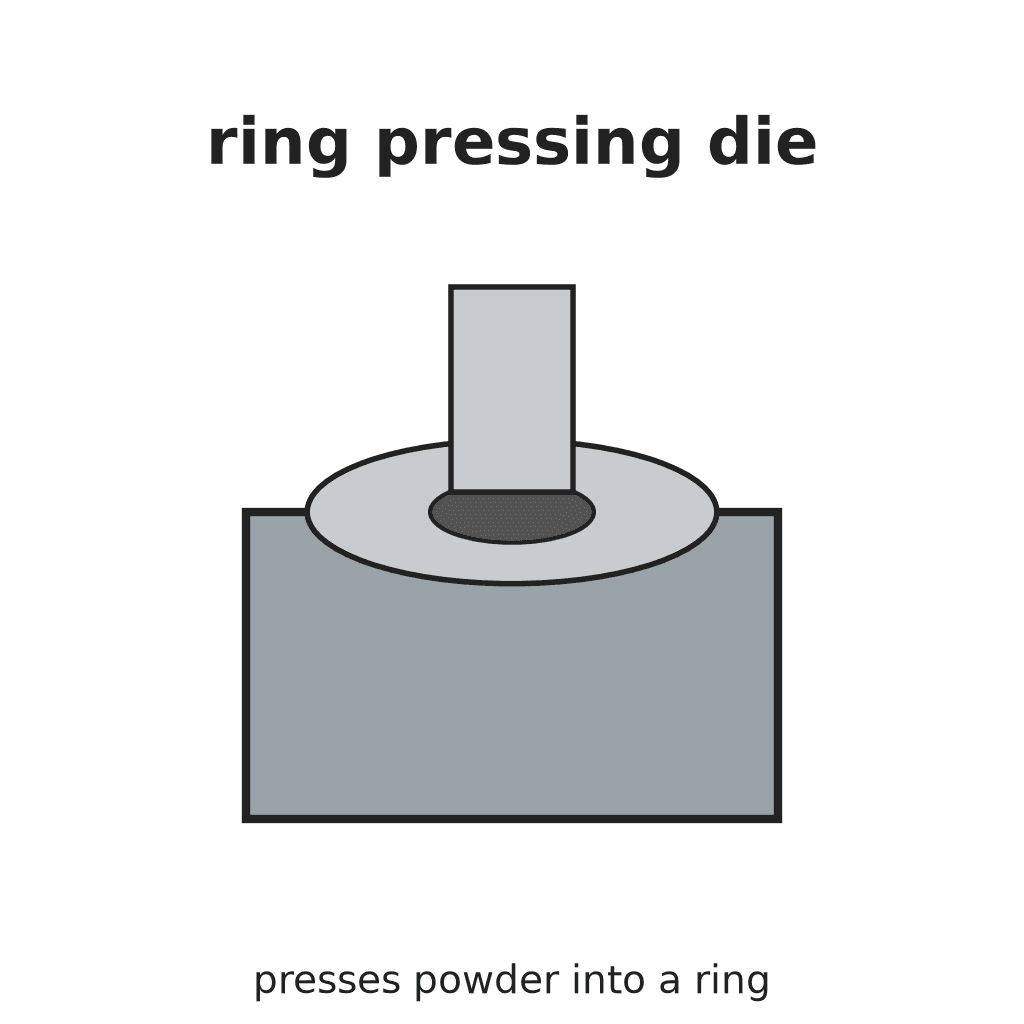
Ring Pressing Die: Core-Rod Die with Tubular Punches and Overfill Filling (Davis & Lemming, GM, US 2,127,994, 1938)
The die set for pressing metal or other powder into rings (bushings, ring cores). A die with a round cavity has a fixed core rod standing up through its middle, so the cavity is ring-shaped; a tube-shaped lower plunger slides up and down round the core rod, and a tube-shaped upper punch comes down to press. Filling is the trick: the lower plunger drops past the pressing point under a shaking shoe of powder, then rises a little to push the surplus back, so every ring gets the same charge with no trapped air.
Result: a die that presses powder into rings of even weight and density, ejected flush with the die top.
Source: J. H. Davis and J. C. Lemming (General Motors), US 2,127,994 (1938). Unknown: steels, sizes, clearances, pressure. Picture: the patent drawing.
Hejuru
Unknown
Amabwiriza
1
1
Make the die, core rod and punches
Make the die, core rod and punches
Make a die block with a straight round cavity open at both ends. Make a core rod that stands up through the middle of the cavity, its top flush with the die top, threaded at its foot to be anchored in the base with a lock nut. Make a tube-shaped lower plunger that slides in the cavity round the core rod, and a tube-shaped upper punch to match. Not given: the steel, sizes, clearances. Ours: tool steel, turned and threaded on the lathe.
Ibikoresho by'iyi ntambwe:
 Inkoni ya kare y'icyuma cy'ibikoresho1 die, core rod, punches
 Icyuma kitazwi1 lock nut
Ibikoresho bikenewe:
 Imashini yo guhinguza icyuma
 Agakoresho ko gukata imizingo y'ibyuma
 Ingano zitazwi
2
2
Harden and finish
Harden and finish
The powder wears the cavity wall, so harden the die and punches and polish the working faces. Not given: the hardening or finish. Ours: a heat-treating oven and quench, then lapping with rouge along the stroke as for the disc die.
Ibikoresho bikenewe:
 Itanura ryo gutunganya hakoreshejwe ubushyuhe
 Indobo yo gukonjesha
 Umutuku w'umucuzi
3
3
Set it in the press
Set it in the press
Fix the die in a heavy table, anchor the core rod in the base through the lower plunger, and drive the lower plunger up and down by a cam lever. Fix the upper punch to the press crosshead. Beside the die, pivot a filling shoe full of powder that can swing over the cavity and shake. Ours: a punch press.
Ibikoresho bikenewe:
 Imashini ikanda itobora
4
4
Fill, press and eject
Fill, press and eject
Start with the lower plunger right up, filling the cavity. Swing the shaking shoe over and lower the plunger: the powder falls in after it by gravity and suction, so no air is trapped. Take the plunger below the pressing position, then raise it to the pressing position, pushing the surplus back into the shoe so every charge is the same. Swing the shoe away, bring down the upper punch to press the ring between the punches, lift the punch and raise the lower plunger to push the ring out flush with the die top; the returning shoe sweeps it aside. Sinter the rings afterwards.
Ibikoresho bikenewe:
Imashini ikanda itoboraIbikoresho
2- 1 die, core rod, punchesUmwanya
- 1 lock nutUmwanya
Ibikoresho bikenewe
7- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
Ibikoresho by'Ibishushanyo Bifitanye Isano
10% igabana
Tool-Steel Bar: Crucible Steel Drawn Out at a Cherry-Red Heat
na Forge
Umucuzi
32
0
0
0
5
0

10% igabana
Building a Screw-Cutting Lathe — The Machine That Makes Other Machines
na Gimli
Ubucuzi bw'Ibyuma
57
0
0
0
4
0

10% igabana
Taps and Dies Cut on the Lathe, with Wrench and Stock
na Martin
Ubucuzi bw'Ibyuma
25
0
0
0
6
0
Iki gishushanyo gikora
CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.