İşbirliği
SANAT
GÜZELLİK & SAĞLIK
ZANAAT
KÜLTÜR & TARİH
EĞLENCE
ÇEVRE
YİYECEK & İÇECEK
TERS MÜHENDİSLİK
BİLİMLER
SPOR
TEKNOLOJİ
GİYİLEBİLİR ÜRÜNLER
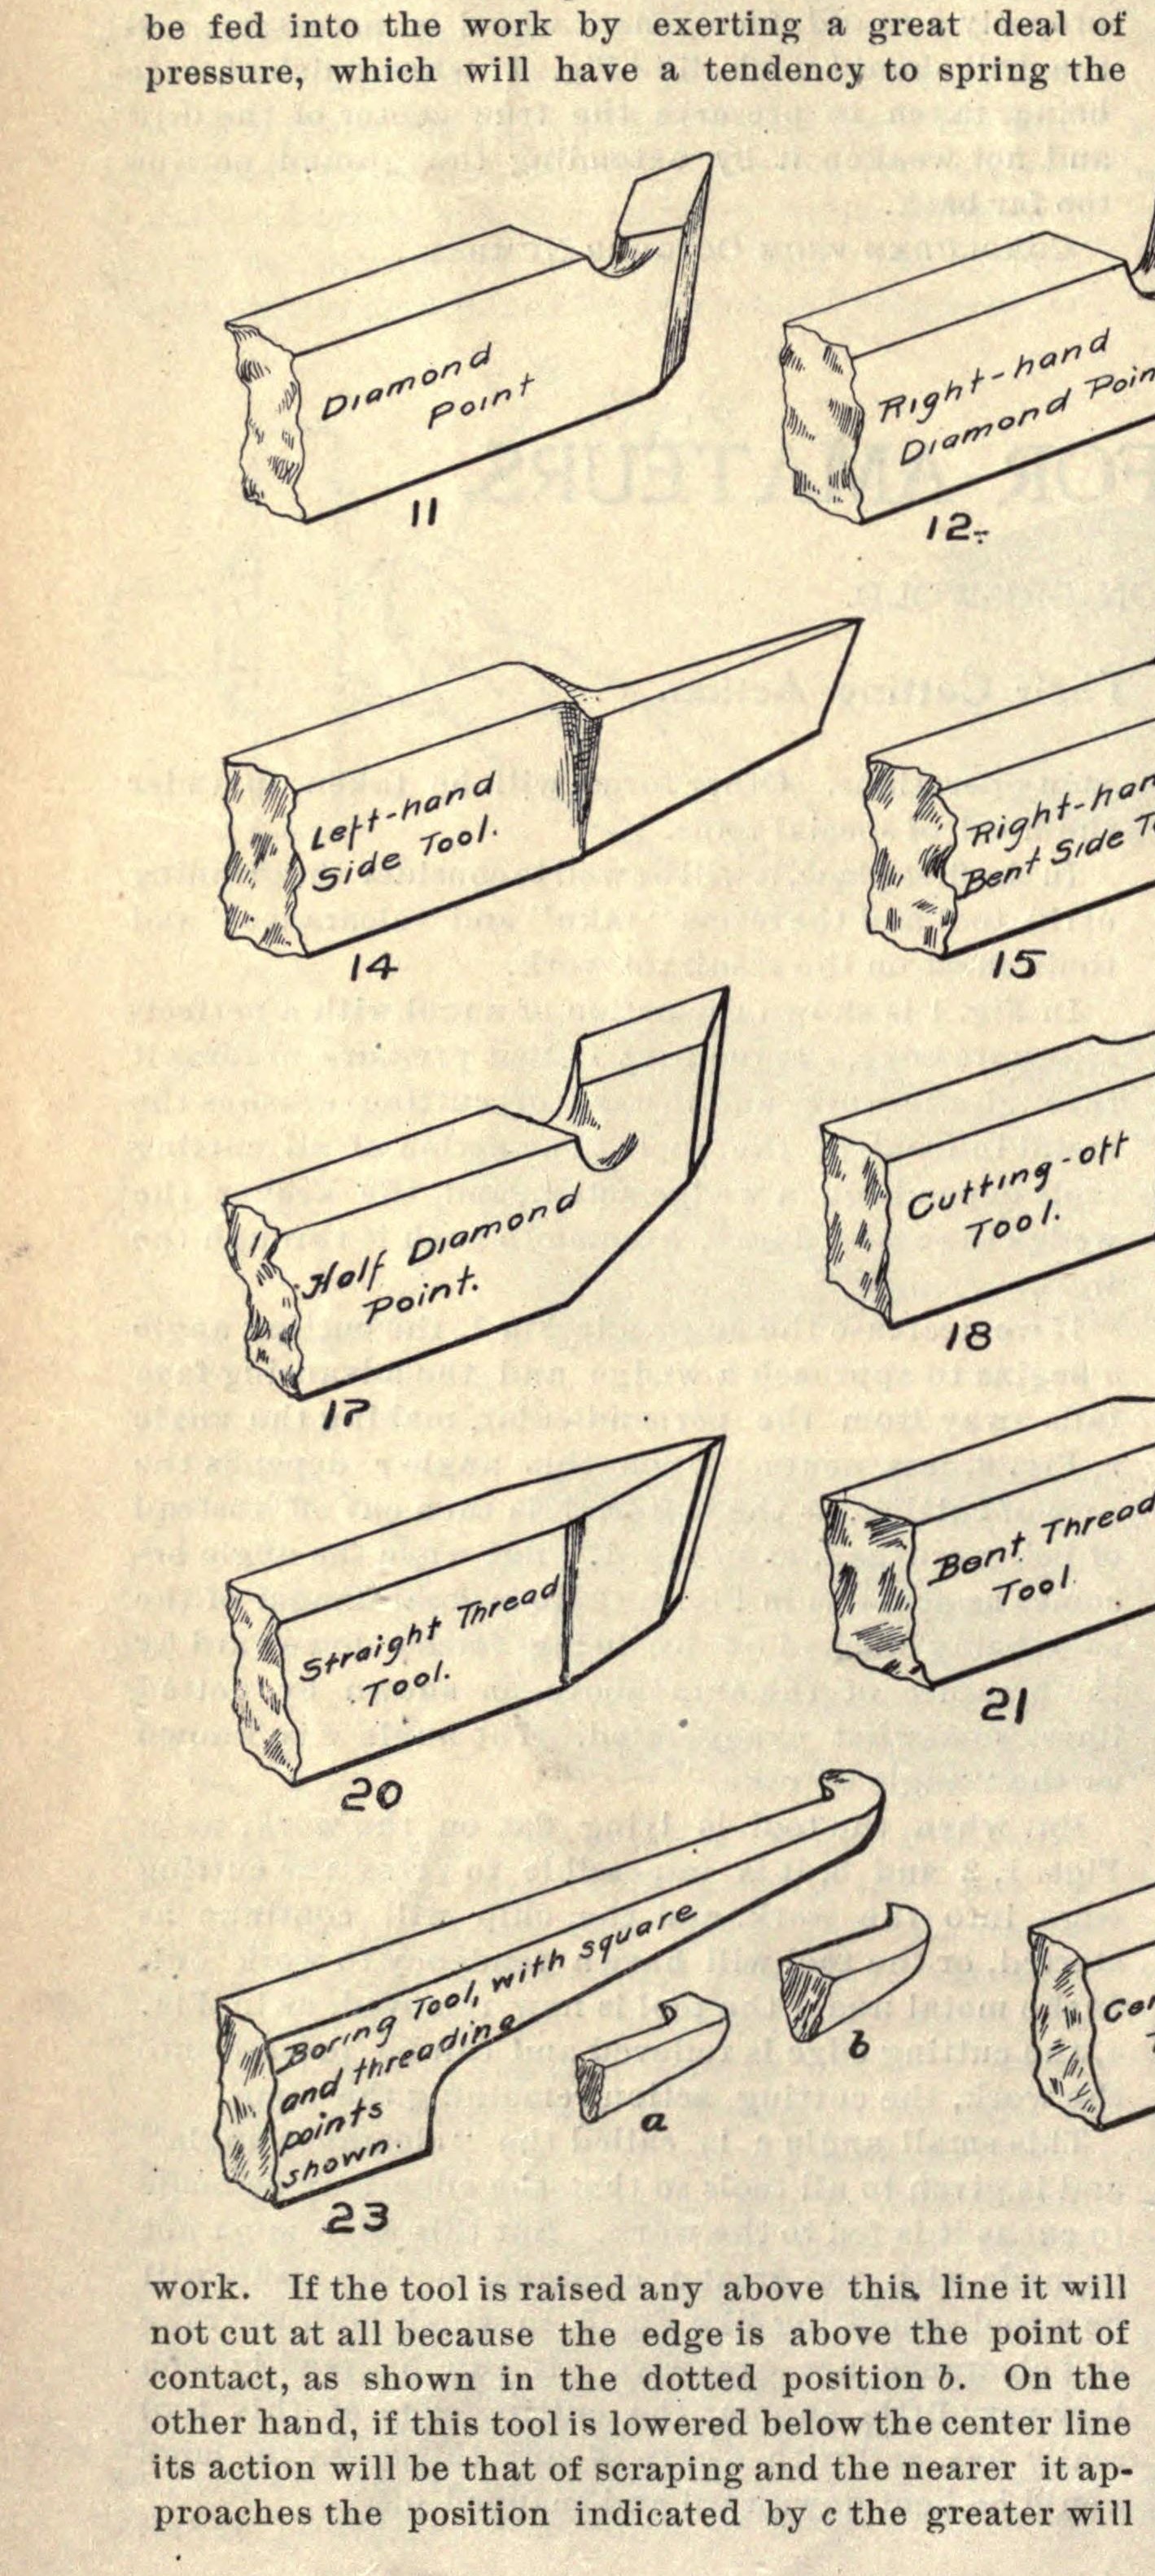

Forged Lathe Tools: Narrow Cutting-Off Tool and Bent-Tip Inside Boring Tool, Ground to Rake and Clearance (Griswold, 1904)
Two of the forged lathe tools in Robert Gibson Griswold's Tool Making for Amateurs (Boston, 1904): a cutting-off (parting) tool deep under a very narrow edge with relieved sides and a chip-splitting groove, and an inside boring and threading tool drawn to a long taper with the tip bent left; both ground to 3-5 degree clearance and the rake suited to the metal.
İleri
Half a day per tool
Talimatlar
1
1
His angles
His angles
Jupyter defteri yükleniyor…
2
2
Read Griswold
Read Griswold
"The writer uses a tool slightly less than 1-16 in. wide and 1 in. deep for short cuts."
3
3
Forge the cutting-off tool
Forge the cutting-off tool
Forge tool steel (stock size ours, to suit your tool post) into a blade deep under the cutting edge, with the point the widest part and the sides relieved behind it so it cannot bind (his fig. 18): slightly under 1/16 in. wide and 1 in. deep for work up to 1/2 in., about 3/32 in. wide for work up to 2 in.
Bu adım için malzemeler:
 Takım çeliği çubuk1 adet
Gerekli aletler:
 Demirci ocağı
 Örs
 Çekiç
 Demirci kerpeteni
4
4
Forge the boring tools
Forge the boring tools
Draw three blanks to a long tapering end and bend the extreme tip to the left (fig. 23).
Bu adım için malzemeler:
Takım çeliği çubuk1 adetGerekli aletler:
Demirci ocağıÖrsÇekiçDemirci kerpeteni5
5
Harden and temper
Harden and temper
Carbon tool steel: harden the ends (ours: cherry red into water) and temper in the yellows. Self-hardening steel must never be quenched in water.
Bu adım için malzemeler:
 Su1 adet
 Zımpara bezi1 adet
Gerekli aletler:
Demirci ocağı Kova
6
6
Grind the cutting-off tool
Grind the cutting-off tool
Give it front and side clearance of 3-5 degrees and little top rake. For larger work grind a round groove in the facing edge so the chip splits into two strings.
Gerekli aletler:
 Taşlama motoru
7
7
Grind the boring points
Grind the boring points
Grind one boring tool as a diamond point, one as a small square point that works into corners, and one as a 60 degree thread point. Rake 3-10 degrees for iron and steel, little or none for brass and copper; hone the edges.
Gerekli aletler:
Taşlama motoru Bileği taşı
8
8
Troubleshooting
Troubleshooting
Lathe tool troubleshooting.
Flow
Loading...
9
9
History and honest limits
History and honest limits
From Robert Gibson Griswold, "Tool Making for Amateurs" IV, **Amateur Work** (Boston), vol. IV (1904-05), pp. 23-26 and figs. 11-25 (checked on the archive.org scan amateurwork04bostrich). He shows a full set (diamond point, side, round-nose, thread, centering, brass tools); this blueprint makes the two our heads need. Stock size and quench are ours.
İlgili Blueprint'ler
Bu blueprint'ler bilgi paylaşır — teknikler, malzemeler veya ilkeler
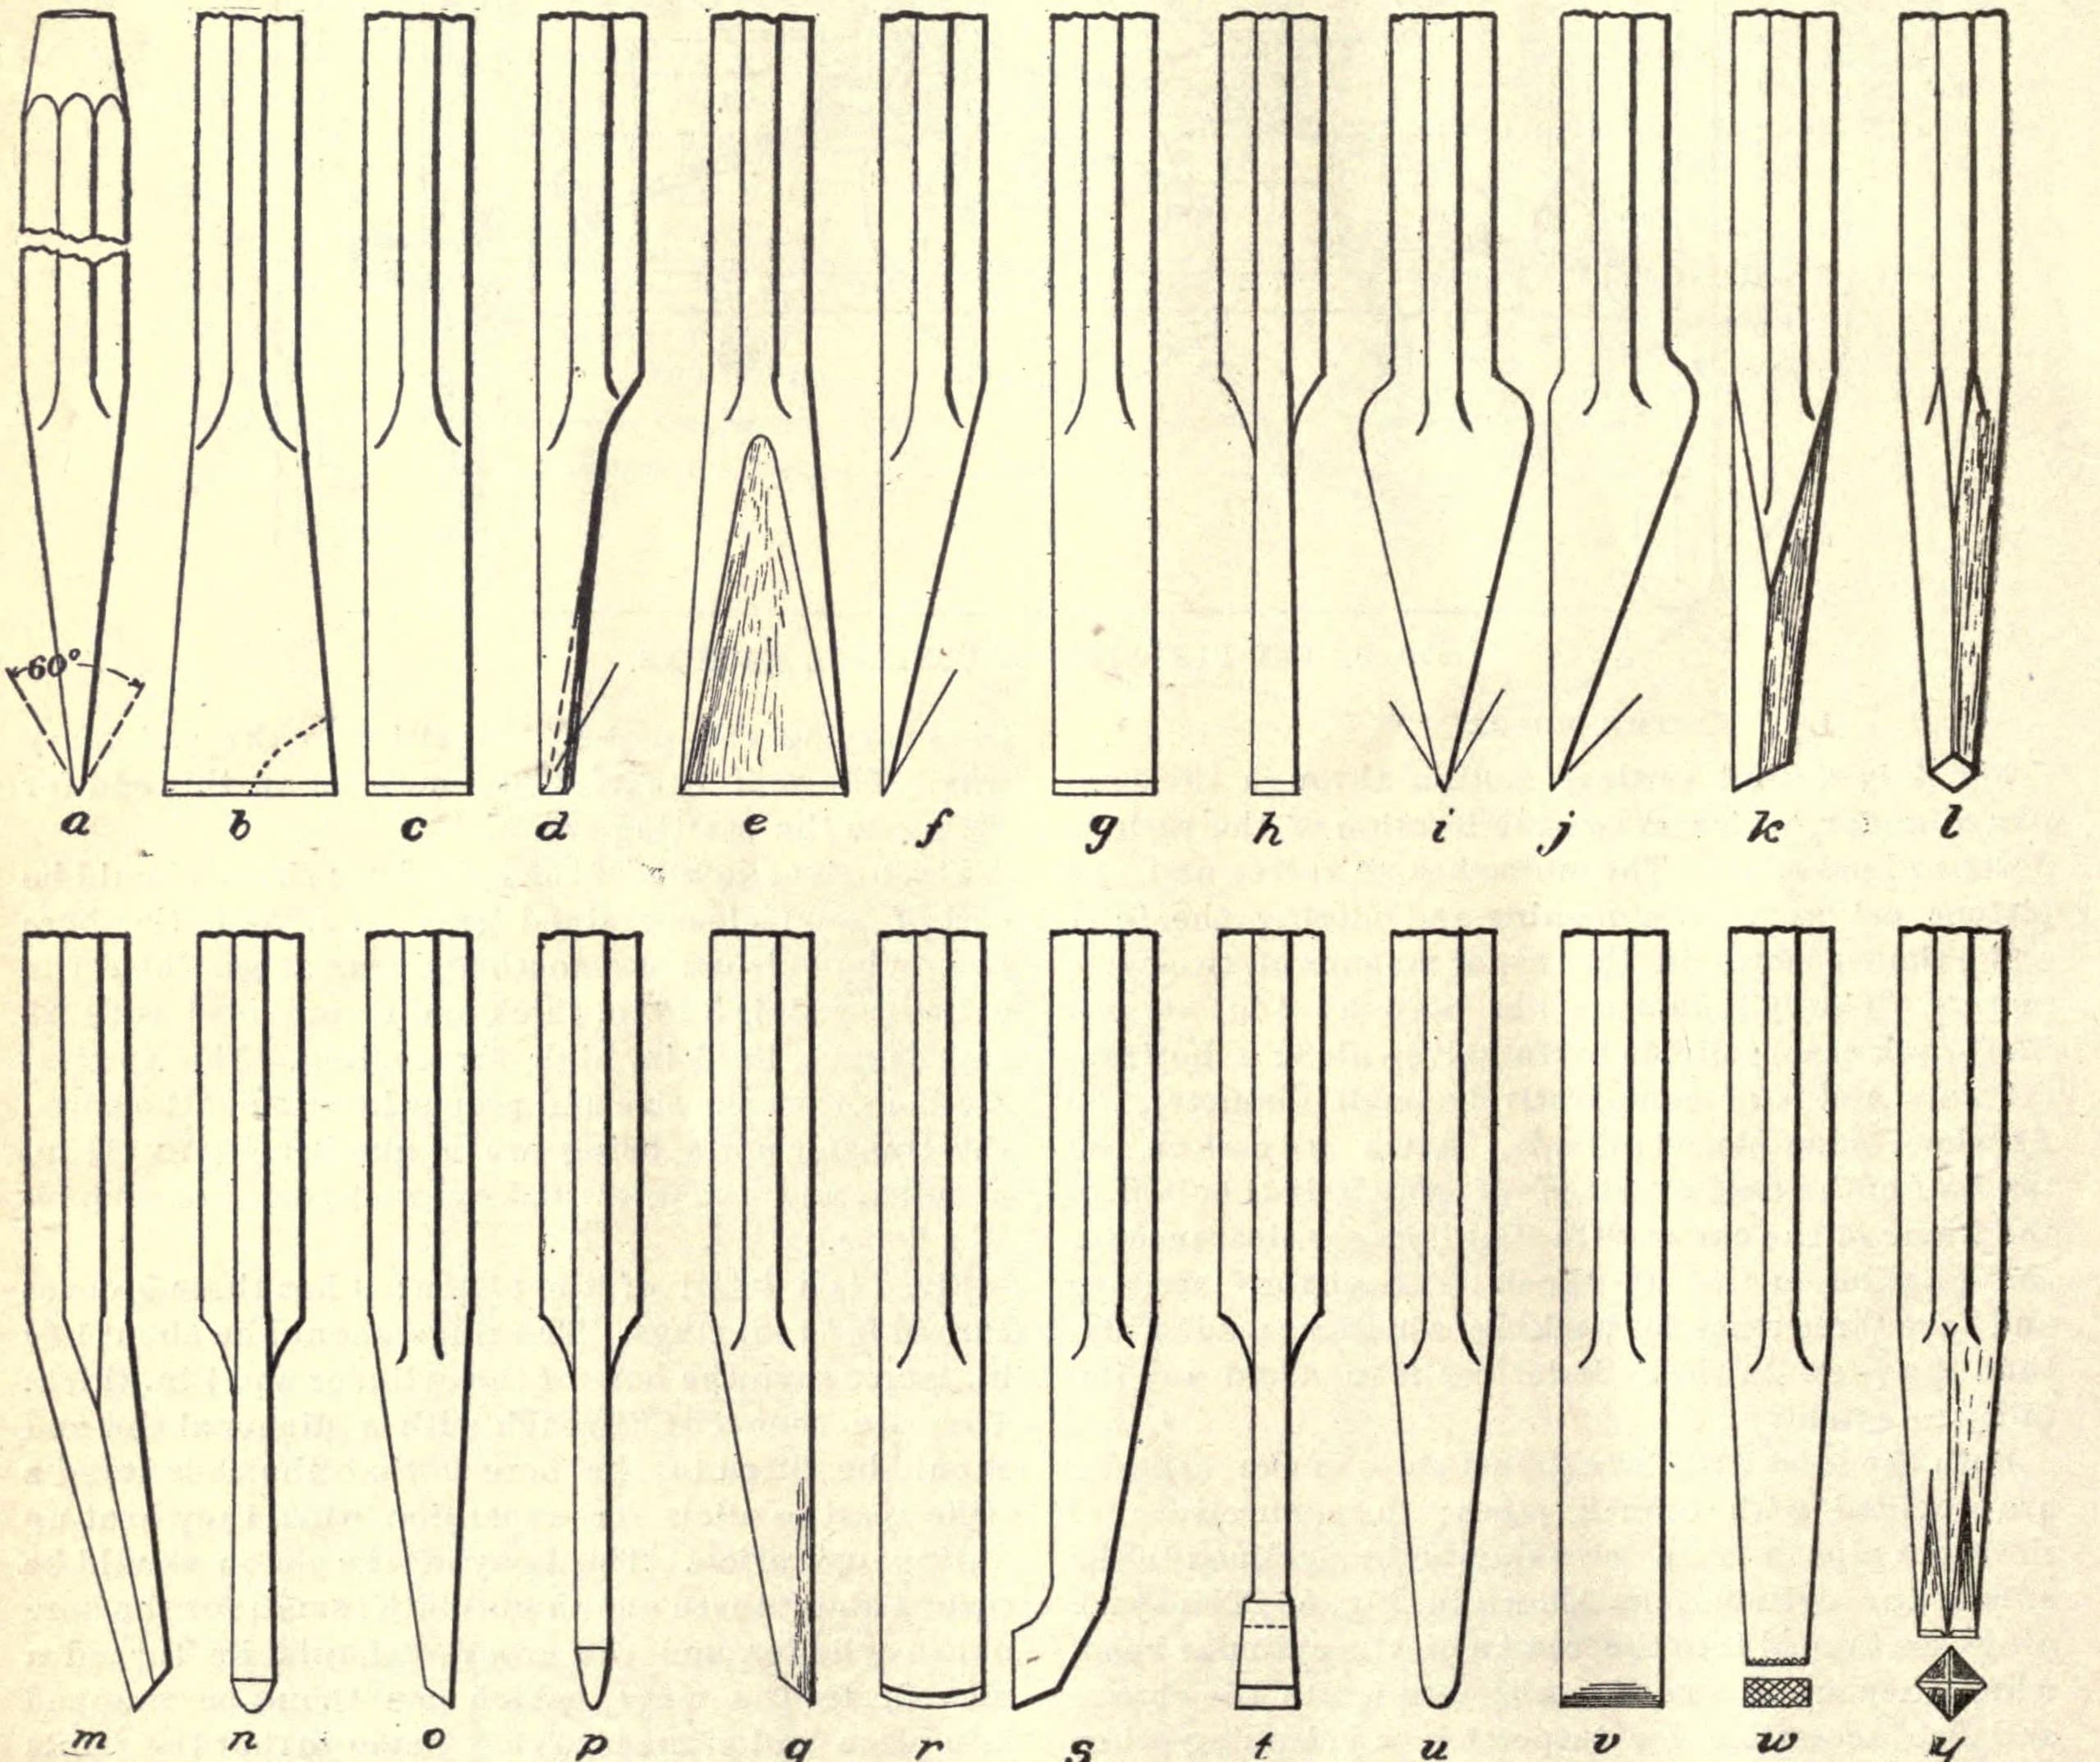
A Set of Cold Chisels: Flat, Gouge, Side, Cape, Diamond-Point and Round-Nose, Edge Hardened Only, Tempered Purple (Griswold, 1904)
Forge tarafından
Metal işleme
11
0
0
0
0
0
Half-Round Taper Reamer: Tool Steel Turned to the Taper, Filed Flat to the Centre Line, Hardened (Griswold, Amateur Work, 1905)
Forge tarafından
Metal işleme
9
0
0
0
0
0
CC0 Kamu Malı
Bu plan CC0 lisansıyla yayınlanmıştır. İzin almadan kopyalayabilir, değiştirebilir, dağıtabilir ve herhangi bir amaçla kullanabilirsiniz.
Planı üzerinden ürün satın alarak Maker'ı destekleyin, böylece Maker Komisyonu Satıcılar tarafından belirlenen komisyonu kazanırlar veya bu Planın yeni bir versiyonunu oluşturun ve gelir paylaşımı için kendi Planınıza bağlantı olarak ekleyin.