МИСТЕЦТВО
КРАСА ТА ЗДОРОВ'Я
РЕМЕСЛО
КУЛЬТУРА ТА ІСТОРІЯ
РОЗВАГИ
СЕРЕДОВИЩЕ
ЇЖА ТА НАПІЇ
ЗБОРНА ІНЖЕНЕРІЯ
НАУК
СПОРТ
ТЕХНОЛОГІЯ
НОСИМО


Pouring Temperature: Too Cold Misruns, Too Hot Tears the Mould
Metal is not poured at its melting point. It is poured at a SUPERHEAT above it — enough that it can travel through the gating and fill the last thin corner before it starts to freeze.
Too little superheat and the metal stops before the cavity is full, or two streams meet and fail to fuse. Too much and it dissolves more gas, oxidises harder, burns the sand, and shrinks more on the way down — so the porosity gets worse rather than better.
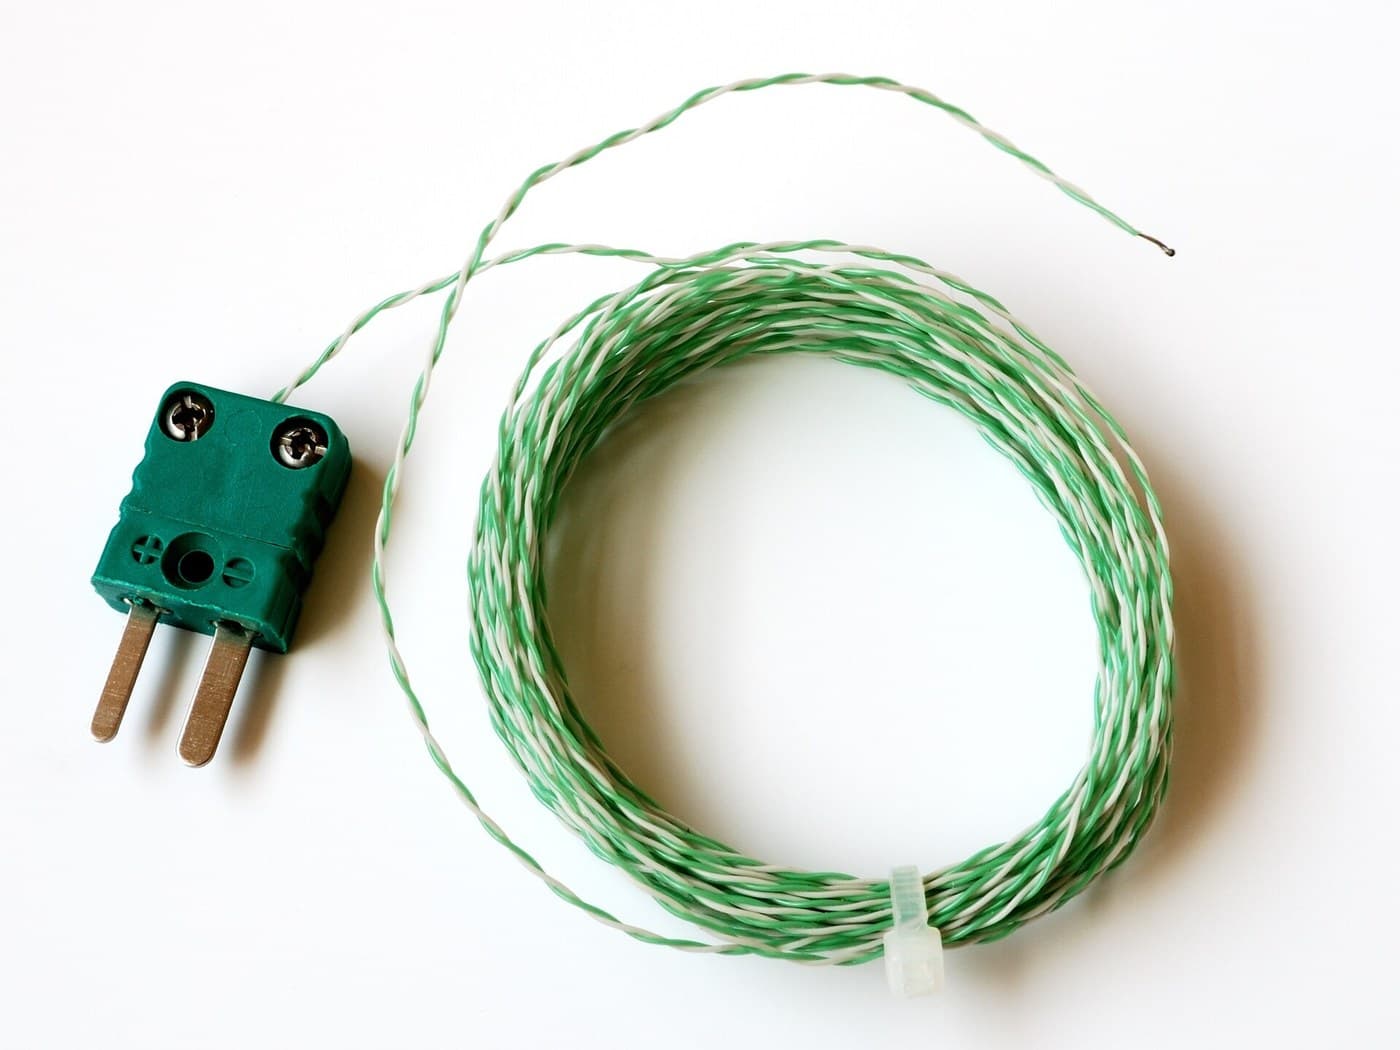
The window is perhaps 100 to 150 degrees wide, it differs by alloy and by casting, and the only way to sit inside it reliably is to MEASURE. Judging melt temperature by colour is the pyrometer rung's warning delivered with molten metal.
Просунутий
3 hours
Інструкції
1
1
Superheat, by alloy
Superheat, by alloy
Завантаження блокнота Jupyter…
Матеріали для цього кроку:
 Бронзовий зливок1 штука
 Алюмінієвий злиток 99,7 % чистоти, 450 г1 штука
Необхідні інструменти ({count})
 Пірометр
 Термопара з індикатором
 Настільний комп'ютер
2
2
Skim, and do not stir the dross back in
Skim, and do not stir the dross back in
Oxide and impurities float. Skim them off the surface of the melt immediately before pouring, with a preheated skimmer, and take them right out of the crucible rather than pushing them aside.
Preheat every tool that will touch molten metal. A cold skimmer or ladle chills the metal locally and, far worse, any trace of moisture on it flashes to steam instantly — which throws metal.
Do not stir after skimming. Stirring folds the remaining surface oxide down into the melt, where it becomes inclusions in the casting. Aluminium is the worst for this: its oxide skin is tough, and every disturbance of the surface makes more of it.
Матеріали для цього кроку:
Бронзовий зливок1 штукаНеобхідні інструменти ({count})
 Шумівка з дрібною сіткою
 Ливарний ківш
 Кліщі для тиглів
 Шкіряні рукавиці з крагами
3
3
Dry everything, and mean it
Dry everything, and mean it
Water and molten metal is the one genuinely dangerous combination in a foundry. Water turned to steam expands roughly 1,600 times, instantly, and if it is under metal it throws that metal outward.
So: preheat and dry the crucible, the tongs, the ladle and every ingot before it goes near the melt. An ingot with condensation on it, or a scrap casting with water trapped in a cavity, is the classic cause.
The mould matters too. Green sand contains water by design and that is fine because it is bound in the clay and the mould is permeable — but a sand that is too wet, or a mould left standing so condensation collects, is the same hazard in a different place.
Матеріали для цього кроку:
Бронзовий зливок1 штука Кускове деревне вугілля1 штука
Необхідні інструменти ({count})
 ТигельКліщі для тиглів
 Затемнені окуляри для горнаШкіряні рукавиці з крагами
4
4
Everything ready before the metal is
Everything ready before the metal is
Once the metal is at temperature it is losing heat and gaining gas every second. The moulds must be closed, weighted, vented and positioned before the crucible comes out of the furnace.
Weight or clamp the cope. Molten metal exerts real upward pressure on the top half of the mould, and an unweighted cope lifts and lets metal run out of the parting line — which is dangerous as well as a lost casting.
Have a clear path, a clear floor, and somewhere planned to put the crucible down. The pour itself takes a few seconds; everything that makes it go well or badly was decided in the minutes before it.
Матеріали для цього кроку:
 Формувальний пісок1 кг
Необхідні інструменти ({count})
 Ливарна опока (верхня та нижня)Кліщі для тиглівЗатемнені окуляри для горнаШкіряні рукавиці з крагами
Матеріали
4- 1 штукаЗаповнювач
- Заповнювач
- 1 штукаЗаповнювач
- Заповнювач
Необхідні інструменти
10- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
Пов'язані креслення
Ці креслення діляться знаннями — техніки, матеріали або принципи



CC0 Суспільне надбання
Це креслення випущено під ліцензією CC0. Ви можете вільно копіювати, змінювати, поширювати та використовувати цю роботу для будь-яких цілей без запиту дозволу.
Підтримайте мейкера, купуючи продукти через його креслення, де він отримує Комісію мейкера встановлену вендорами, або створіть нову ітерацію цього креслення та включіть його як зв'язок у власне креслення для розподілу доходу.