NGHỆ THUẬT
LÀM ĐẸP VÀ SỨC KHỎE
THỦ CÔNG
VĂN HÓA VÀ LỊCH SỬ
GIẢI TRÍ
MÔI TRƯỜNG
THỰC PHẨM VÀ ĐỒ UỐNG
KỸ THUẬT NGƯỢC
KHOA HỌC
THỂ THAO
CÔNG NGHỆ
THIẾT BỊ ĐEO
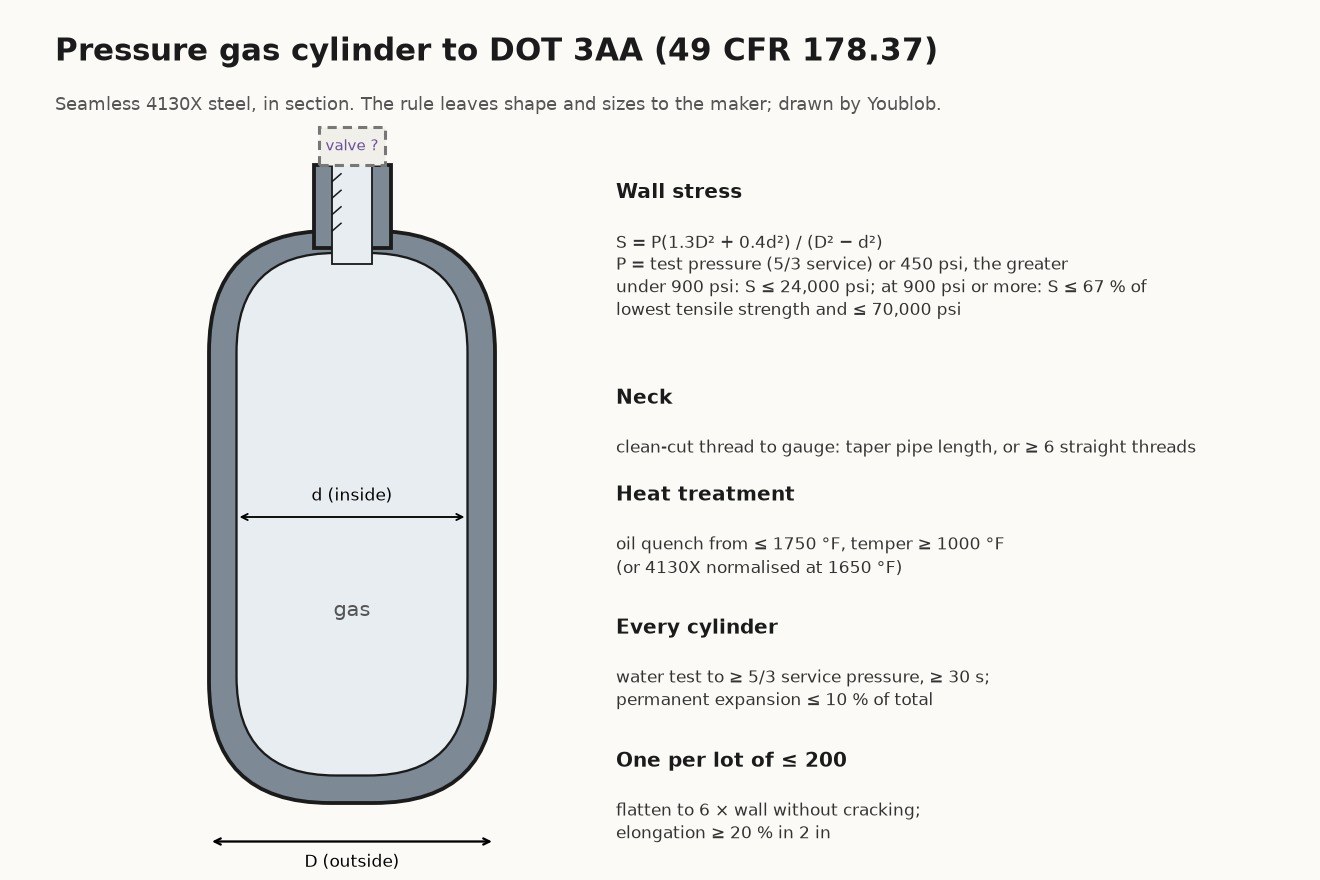


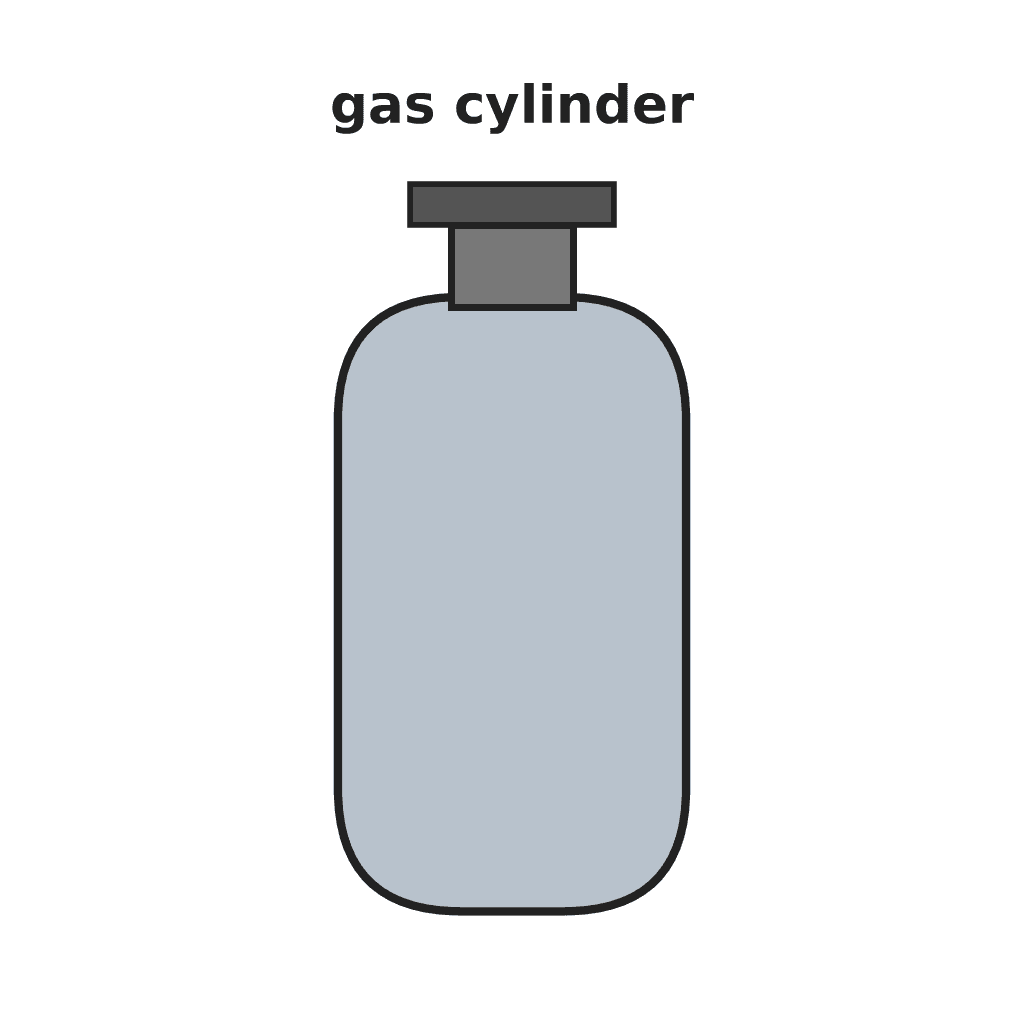
Pressure Gas Cylinder: Seamless 4130X Steel to DOT 3AA (49 CFR 178.37)
A seamless steel cylinder for compressed or liquefied gas, made to the US rule DOT 3AA: at least 150 psi service pressure, up to 1,000 lb of water capacity. The rule gives the steel, a formula for the wall, the heat treatment and the tests every cylinder or lot must pass. It does not say how the shell is formed.
Result: a seamless 4130X steel cylinder, heat-treated and proof-tested to 5/3 of its service pressure, with a threaded neck for its valve.
Source: 49 CFR 178.37, Specification 3AA. Unknown: how the shell is formed, the valve, the test apparatus. Picture drawn by Youblob.
Nâng cao
Unknown
Hướng dẫn
1
1
Size the wall
Size the wall
Pick the service pressure (at least 150 psi) and the diameter. Find the wall stress S = P(1.3D² + 0.4d²) / (D² − d²), with D and d the outside and inside diameters in inches and P the test pressure (5/3 of service pressure) or 450 psi, whichever is greater. Below 900 psi service, S may not pass 24,000 psi, and a cylinder over 5 in across needs a wall of at least 0.100 in. At 900 psi or more, S may not pass 67 % of the steel's lowest tensile strength, nor 70,000 psi.
Công cụ cần thiết:
 Kích thước chưa rõ
2
2
Get the steel
Get the steel
Use open-hearth, basic oxygen or electric steel of uniform quality, here 4130X: carbon 0.25-0.35 %, manganese 0.40-0.90 %, silicon 0.15-0.35 %, chromium 0.80-1.10 %, molybdenum 0.15-0.25 %, phosphorus 0.04 % and sulphur 0.05 % at most. For hot-drawn cylinders, mark each billet with its heat number.
Vật liệu cho bước này:
 Phôi thép 41301 per cylinder
Công cụ cần thiết:
Kích thước chưa rõ3
3
Form the seamless shell
Form the seamless shell
Form the billet into a seamless cylinder with no fissures and a smooth, even surface; machine away any defects. A bottom closed by welding or spinning must be at least twice the minimum wall thick. Do not weld anything else, except neck and foot rings on cylinders of 500 psi or less. Not given: how the shell is formed (the rule names hot drawing from billet or plate, and spinning).
Công cụ cần thiết:
 Phương pháp tạo hình chưa rõKích thước chưa rõ
4
4
Thread the neck
Thread the neck
Cut a clean, even thread in the neck opening, to gauge. A taper thread must be at least as long as an American Standard taper pipe thread. A straight thread needs at least six engaged threads, a tight fit, a gasket, and a shear strength of at least ten times the test pressure.
Công cụ cần thiết:
 Bộ ta-rô và bàn ren
5
5
Heat-treat
Heat-treat
Heat-treat each finished cylinder evenly before testing. Quench it in oil or another suitable medium from the temperature right for the steel, no higher than 1750 °F, then temper at 1000 °F or more. Or normalise 4130X at 1650 °F instead, with no tempering. A cylinder quenched in water, or in anything cooling more than 80 % as fast, must be checked for quench cracks by magnetic particle, dye penetrant or ultrasound; a cracked one is scrapped.
Công cụ cần thiết:
 Lò nhiệt luyện
 Bể tôi dầu
 Lò ram
6
6
Pressure-test every cylinder
Pressure-test every cylinder
Test each cylinder with water by the water-jacket or direct-expansion method of CGA C-1, to at least 5/3 of service pressure, held for at least 30 seconds and until it stops expanding. Between heat treatment and this test, never go above 90 % of test pressure. The permanent expansion may not pass 10 % of the total expansion. Not given: the CGA C-1 apparatus.
Công cụ cần thiết:
 Bộ thử áp suất thủy lực
7
7
Test one from each lot
Test one from each lot
From each lot of 200 or fewer, take one cylinder. Flatten it between two 60° knife edges rounded to ½ in radius, set across its axis: it must reach six times the wall thickness without cracking. Cut two tensile specimens from it: find the yield at 0.2 % offset, moving the cross-head no faster than ⅛ in per minute, and the tensile strength; elongation must be at least 20 % over 2 in (10 % on other gauge lengths). A rejected cylinder may be heat-treated again and retested, never repaired by welding or spinning.
Công cụ cần thiết:
 Máy ép thủy lực
 Máy thử vật liệu
8
8
Fit the valve
Fit the valve
Screw the valve into the threaded neck. A cylinder whose bottom was closed by spinning or by a plug must also pass a gas leak test: apply at least service pressure to one side of the clean, dry bottom for at least a minute, with the other side under water, and reject it at any leak. Not given: the valve.
Vật liệu cho bước này:
 Van chưa rõ1 cái
Công cụ cần thiết:
 Mỏ lết
Vật liệu
2- 1 per cylinderTạm thời
- 1 cáiTạm thời
Công cụ yêu cầu
10- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
Vật liệu bản thiết kế liên kết


Bản thiết kế này làm ra
Blueprint liên quan
Các blueprint này chia sẻ kiến thức — kỹ thuật, vật liệu hoặc nguyên tắc
CC0 Phạm vi công cộng
Bản thiết kế này được phát hành theo CC0. Bạn tự do sao chép, sửa đổi, phân phối và sử dụng cho bất kỳ mục đích nào mà không cần xin phép.
Hỗ trợ nhà sáng tạo bằng cách mua sản phẩm qua bản thiết kế, nơi họ nhận Hoa hồng nhà sáng tạo do nhà bán hàng đặt, hoặc tạo phiên bản mới và kết nối trong bản thiết kế riêng để chia sẻ doanh thu.