NGHỆ THUẬT
LÀM ĐẸP VÀ SỨC KHỎE
THỦ CÔNG
VĂN HÓA VÀ LỊCH SỬ
GIẢI TRÍ
MÔI TRƯỜNG
THỰC PHẨM VÀ ĐỒ UỐNG
KỸ THUẬT NGƯỢC
KHOA HỌC
THỂ THAO
CÔNG NGHỆ
THIẾT BỊ ĐEO
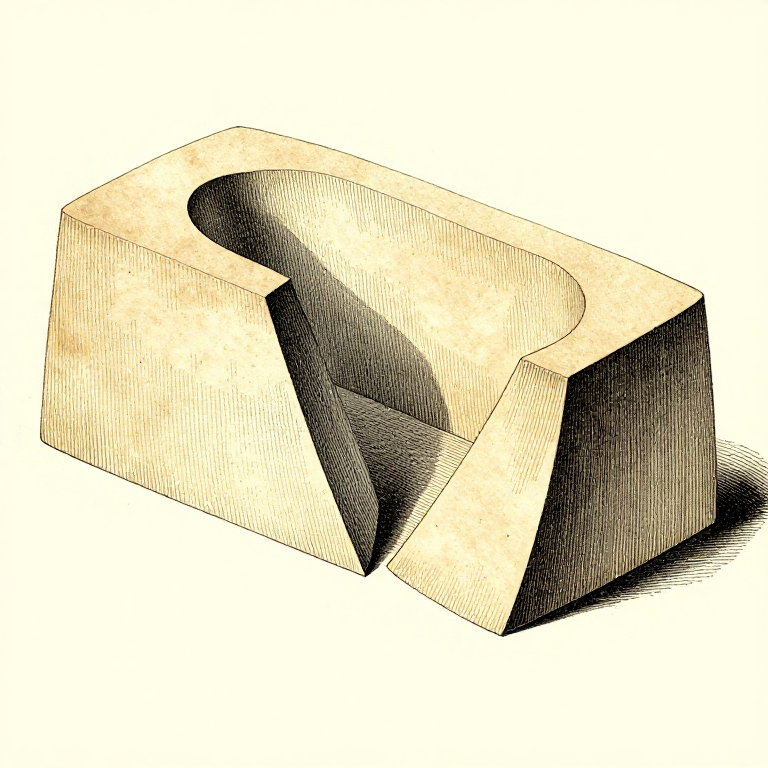

The Pattern Is Not the Part: Draft, Shrinkage and Machining Allowance
A pattern is not a copy of the finished part. It is deliberately LARGER, deliberately TAPERED, and deliberately oversized wherever a machined surface will be cut — and each of those three differences has a separate reason.
DRAFT is the taper that lets the pattern come out of the sand without tearing the mould. SHRINKAGE allowance makes the pattern bigger because metal contracts as it freezes and cools. MACHINING allowance leaves metal for the cutting tool to remove.
Get any of the three wrong and the casting is scrap. Get them right and the same pattern makes identical parts indefinitely, which is the entire economic point of casting.
Trung cấp
3 hours
Hướng dẫn
1
1
Draft: the pattern has to come out
Draft: the pattern has to come out
Every surface that runs perpendicular to the parting plane must be tapered so the pattern lifts cleanly. A vertical wall drags sand with it and leaves a torn mould, and that tear becomes a lump on the casting.
One to three degrees is usual for sand casting, more for deep pockets and less for shallow ones. The rule of thumb is that a deeper draw needs more draft, because a small angle over a long distance still leaves the sand gripping.
Draft always ADDS material away from the parting line, never removes it. A part that must be a precise size at the bottom of a deep feature has to be machined there, because draft is not optional and it is always in the direction that makes the casting thicker.
Vật liệu cho bước này:
 Tấm gỗ cứng1 cái
 Cát đúc1 kg
Công cụ cần thiết:
 Bộ giũa
 Thước cặp điện tử 6 inch
 Thước kẻ
2
2
Shrinkage: build the pattern oversize by the right amount
Shrinkage: build the pattern oversize by the right amount
Đang tải sổ tay Jupyter…
Vật liệu cho bước này:
Tấm gỗ cứng1 cái Thỏi đồng thanh1 cái
Công cụ cần thiết:
 Máy tính để bànThước cặp điện tử 6 inchThước kẻ
3
3
Machining allowance goes only where a tool will cut
Machining allowance goes only where a tool will cut
A cast surface is rough, slightly scaled, and not accurately placed. Any face that has to be flat, parallel or dimensionally exact must be machined, and the pattern has to carry extra metal there for the tool to remove.
Two to five millimetres is typical for sand casting, and more on large surfaces and on the cope side — the upper half of the mould collects more inclusions, so critical machined faces are placed in the drag where possible.
Do NOT add it everywhere. Extra metal is extra weight, extra cost, extra shrinkage to feed, and extra machining time. Deciding which faces are machined and which are left as-cast is a design decision made before the pattern is started.
Vật liệu cho bước này:
Tấm gỗ cứng1 cáiCông cụ cần thiết:
Thước cặp điện tử 6 inchBộ giũa4
4
Finish the pattern properly, because it prints
Finish the pattern properly, because it prints
Every scratch, dent and grain on the pattern is reproduced in the sand and then in the metal. A pattern sanded smooth and sealed gives a smooth casting; a rough one gives a rough one, and rough castings are harder to clean and harder to machine.
Seal and wax wooden patterns. Bare wood absorbs moisture from green sand, swells and changes size, and it also grips the sand instead of releasing.
Fillet every internal corner. A sharp internal corner in the pattern makes a sharp sand edge that breaks off into the casting, and it makes a stress concentration in the finished part — the same argument as a fillet in a printed part or a forged one.
Vật liệu cho bước này:
Tấm gỗ cứng1 cái Sáp ong1 cái
Công cụ cần thiết:
Bộ giũa Kính lúp thợ kim hoànThước cặp điện tử 6 inch
Vật liệu
4- 1 cáiTạm thời
- 1 kgTạm thời
- 1 cáiTạm thời
- 1 cáiTạm thời
Blueprint liên quan
Các blueprint này chia sẻ kiến thức — kỹ thuật, vật liệu hoặc nguyên tắc
Carving a Stone Mould for Bronze Casting — Open-Face and Bivalve Moulds
bởi Forge
Gia công kim loại
69
0
0
0
3
0
Casting a Bronze Socketed Spearhead — Bivalve Mould Method
bởi Forge
Gia công kim loại
37
0
0
0
1
0
Fits: Clearance, Transition and Interference — the Difference Is Microns
bởi Martin
Dụng cụ gia công kim loại
25
0
0
0
0
0
CC0 Phạm vi công cộng
Bản thiết kế này được phát hành theo CC0. Bạn tự do sao chép, sửa đổi, phân phối và sử dụng cho bất kỳ mục đích nào mà không cần xin phép.
Hỗ trợ nhà sáng tạo bằng cách mua sản phẩm qua bản thiết kế, nơi họ nhận Hoa hồng nhà sáng tạo do nhà bán hàng đặt, hoặc tạo phiên bản mới và kết nối trong bản thiết kế riêng để chia sẻ doanh thu.