ARTE
BELLEZZA E BENESSERE
MESTIERE
CULTURA E STORIA
DIVERTIMENTO
AMBIENTE
CIBO E BEVANDE
INGEGNERIA INVERSA
SCIENZE
SPORT
TECNOLOGIA
INDOSSABILI
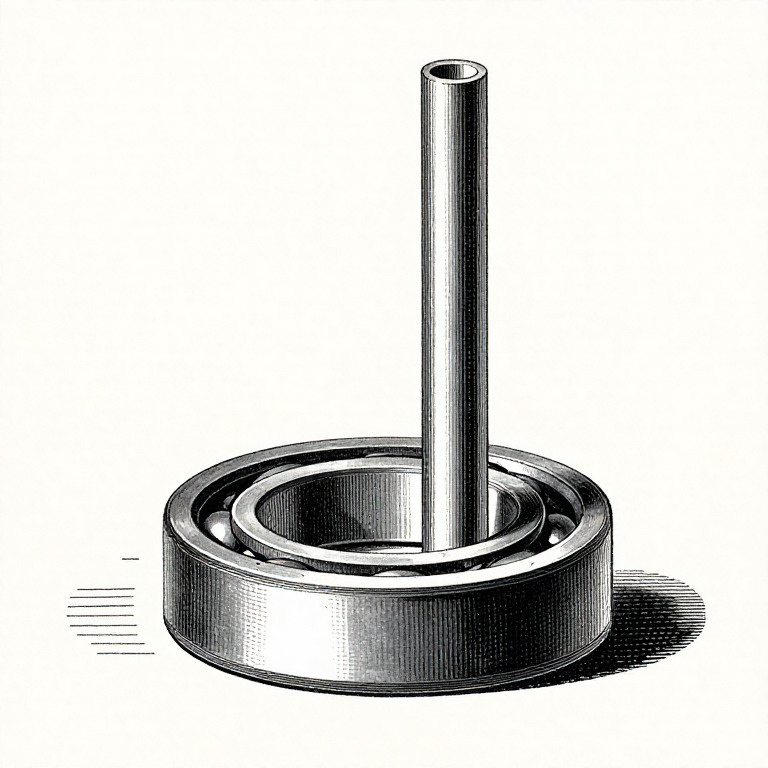

Mounting a Bearing: Press on the Ring That Is Being Fitted, Never Through the Balls
A rolling bearing has a load path: from one ring, through the rolling elements, to the other ring. Mounting force must never take that path, because the balls and the raceways are hardened to carry a rolling load and not a hammer blow.
Press on the inner ring when fitting to a shaft. Press on the outer ring when fitting into a housing. Drive through the wrong ring and the force goes through the balls, leaving tiny dents in the raceway — BRINELLING — that the bearing then runs over thousands of times a minute.
The damage is invisible on the bench and unmistakable in service: a new bearing that rumbles, gets hot, and fails early. It is the commonest way a perfectly good bearing is destroyed before it ever turns.
Intermedio
2 hours
Istruzioni
1
1
Everything clean, and the bearing last out of its wrapper
Everything clean, and the bearing last out of its wrapper
A bearing's working clearance is measured in microns, so a particle of grit is a boulder. Clean the shaft, the housing, the tools and your hands before the bearing comes out of its packet.
Leave it wrapped until the moment it goes on. The protective oil on a new bearing is there for storage and is compatible with most greases, so it does not need washing off unless the instructions say so — and washing it off usually introduces more contamination than it removes.
Inspect the seat rather than the bearing. Burrs, nicks and old adhesive on a shaft shoulder will hold the bearing crooked, and a bearing that is 0.05 mm out of square is being asked to run misaligned for its whole life.
Materiali per questo passaggio:
 Sgrassatore (a base di agrumi)1 pezzo
Strumenti necessari:
 Guanti in nitrile
 Calibro a corsoio
 Quaderno
2
2
Force on the correct ring, square and steady
Force on the correct ring, square and steady
Fitting to a SHAFT: the inner ring is the interference fit, so all force goes on the inner ring. Use a tube or a bearing fitting tool that touches only that ring.
Fitting into a HOUSING: the outer ring is the fit, so all force goes on the outer ring. If a bearing must go onto a shaft and into a housing at the same time, the tool must contact BOTH rings simultaneously.
Press steadily rather than hammering. A press or a threaded drawbar applies an even, square, controlled force; a hammer applies a sudden one at whatever angle it lands. If a hammer is unavoidable, hit a proper fitting tool and never the bearing, and never the balls.
Materiali per questo passaggio:
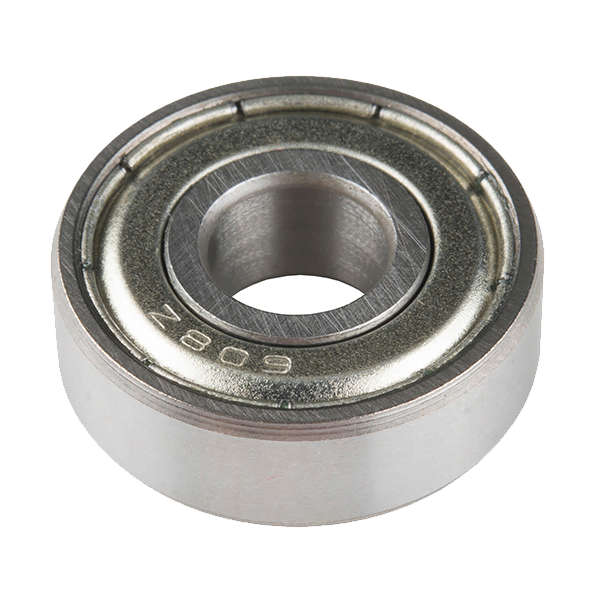 Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)1 pezzo
 Albero d'acciaio da 30 mm1 pezzo
Strumenti necessari:
 Morsa da banco pesante
 Mazzuolo di gomma
 Riga di riscontro
3
3
Seat it fully against the shoulder, and check
Seat it fully against the shoulder, and check
A bearing that stops a fraction short of its shoulder will be pushed the rest of the way by the first axial load it meets — after everything else has been assembled and set.
Check with a feeler gauge all the way round between the ring and the shoulder. All round matters: a gap on one side only means it is going on crooked, and further pressing will make that worse rather than better.
Then turn it by hand. A correctly mounted bearing turns smoothly with no notches and no tight spots. Roughness at this stage is either contamination, a crooked fit, or an interference so tight that it has squeezed the internal clearance out — and all three are cheaper to fix now than later.
Materiali per questo passaggio:
Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)1 pezzoStrumenti necessari:
 Serie di spessimetri
 Comparatore a quadranteRiga di riscontro
4
4
Internal clearance: the fit eats it
Internal clearance: the fit eats it
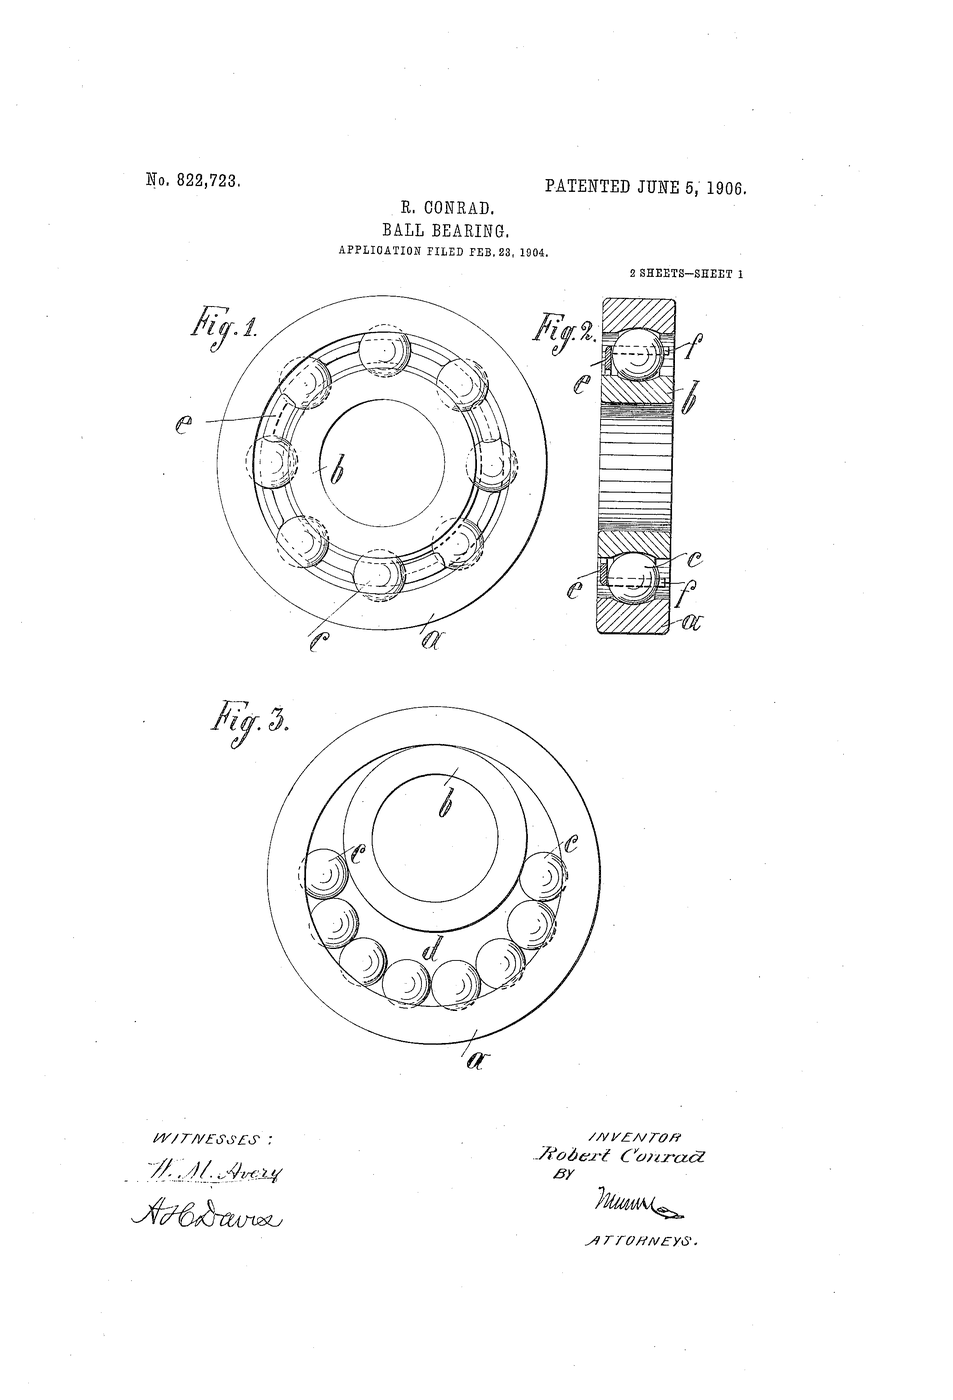
A ball bearing is made with a small gap between the balls and the raceways. Press the inner ring onto an oversized shaft and the ring stretches, closing that gap — a 15 micron interference can remove most of a standard bearing's clearance.
Then the machine warms up. The inner ring is closer to the shaft and usually hotter than the outer, so it expands more and closes the gap further. A bearing with no clearance left is preloaded by accident, runs hot, and fails fast.
That is what the C3 and C4 markings mean: bearings made with extra internal clearance for exactly these situations — tight fits, hot shafts, or both. Choosing one is not a precaution, it is the correct part for the conditions.
Materiali per questo passaggio:
Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)1 pezzo Cuscinetti a sfere1 pezzo
Strumenti necessari:
 Calibro digitale da 6 polliciQuadernoSerie di spessimetri
Materiali
4- Segnaposto
- Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)10% commissione1 pezzo€1.12
- 1 pezzoSegnaposto
- 1 pezzoSegnaposto
Strumenti richiesti
9- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
Totale stimato
Ciò che il maker ha acquistato. I materiali senza prezzo si trovano dove li compri tu.
Blueprint correlati
Questi blueprint condividono conoscenze — tecniche, materiali o principi
CC0 Pubblico dominio
Questo progetto è rilasciato sotto CC0. Sei libero di copiare, modificare, distribuire e utilizzare quest'opera per qualsiasi scopo, senza chiedere permesso.
Supporta il Maker acquistando prodotti tramite il suo progetto dove guadagna una Commissione Maker stabilita dai venditori, oppure crea una nuova iterazione di questo progetto e includilo come collegamento nel tuo progetto per condividere i ricavi.