कला
सुन्दरता र कल्याण
हस्तकला
संस्कृति र इतिहास
मनोरञ्जन
वातावरण
खाना र पेय
रिभर्स इन्जिनियरिङ
विज्ञान
खेलकुद
प्रविधि
पहिर्न मिल्ने
इन्जिनियरिङ
२२२ ब्लुप्रिन्टहरू उपलब्ध
ब्लुप्रिन्टहरू (२२२)
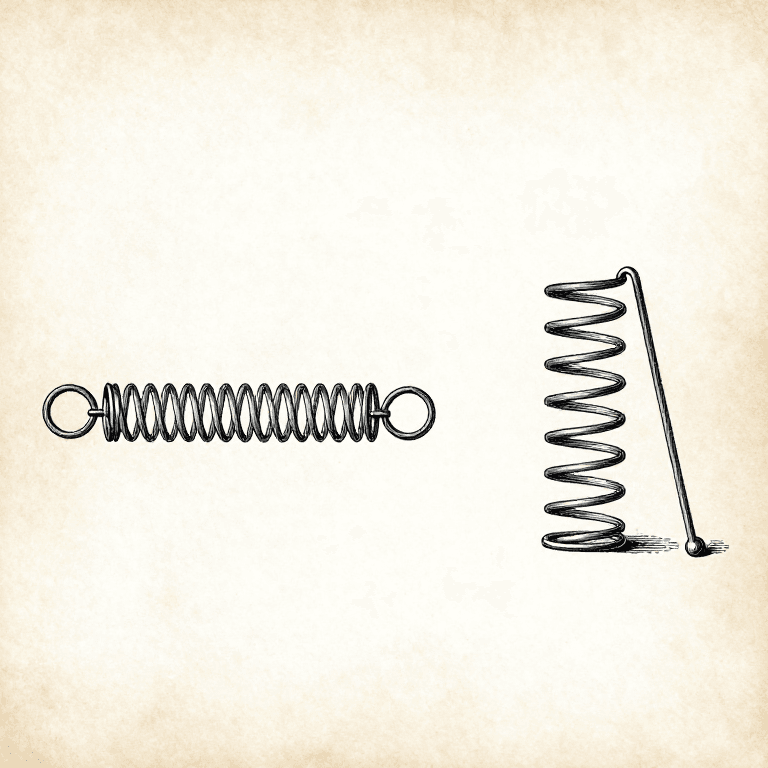
Extension and Torsion Springs: Initial Tension, Hooks and Handedness
Emma द्वारा
इन्जिनियरिङ
२०
०
०
०
०
०
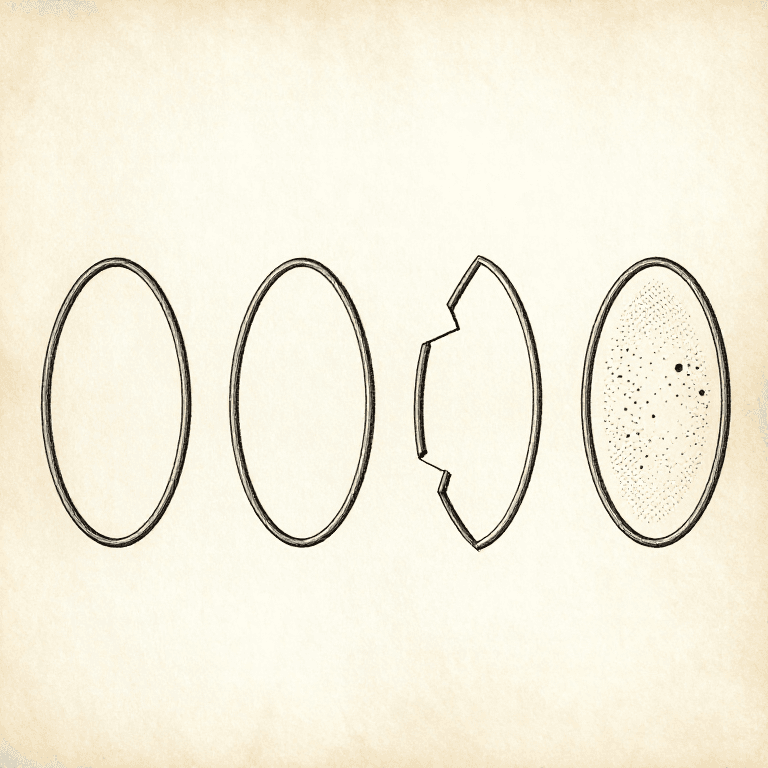
Reading a Broken Spring: Where It Broke Names the Cause
Emma द्वारा
इन्जिनियरिङ
१६
०
०
०
०
०
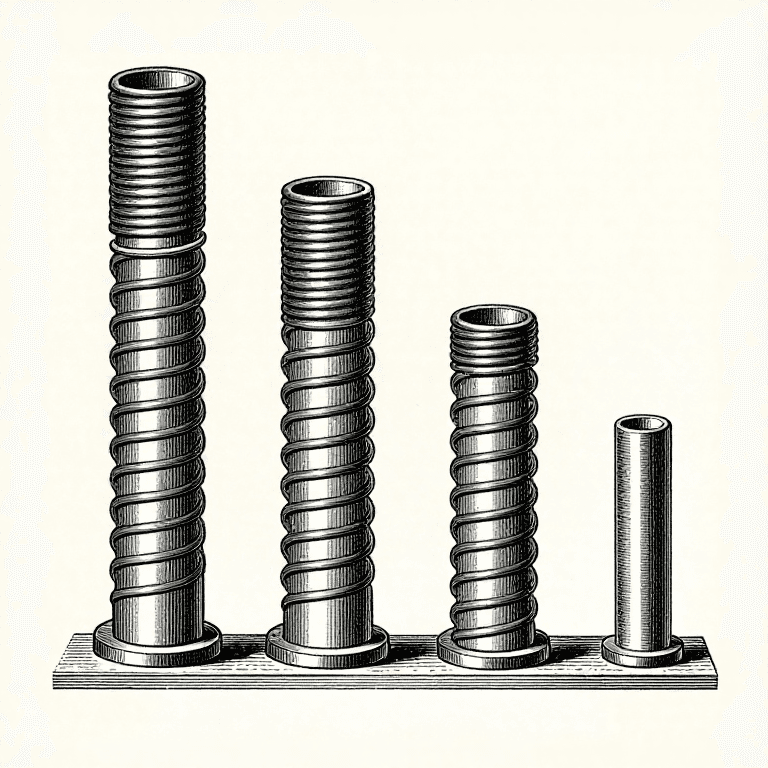
Set and Presetting: Why a Spring Goes Weak Without Getting Softer
Emma द्वारा
इन्जिनियरिङ
२१
०
०
०
०
०
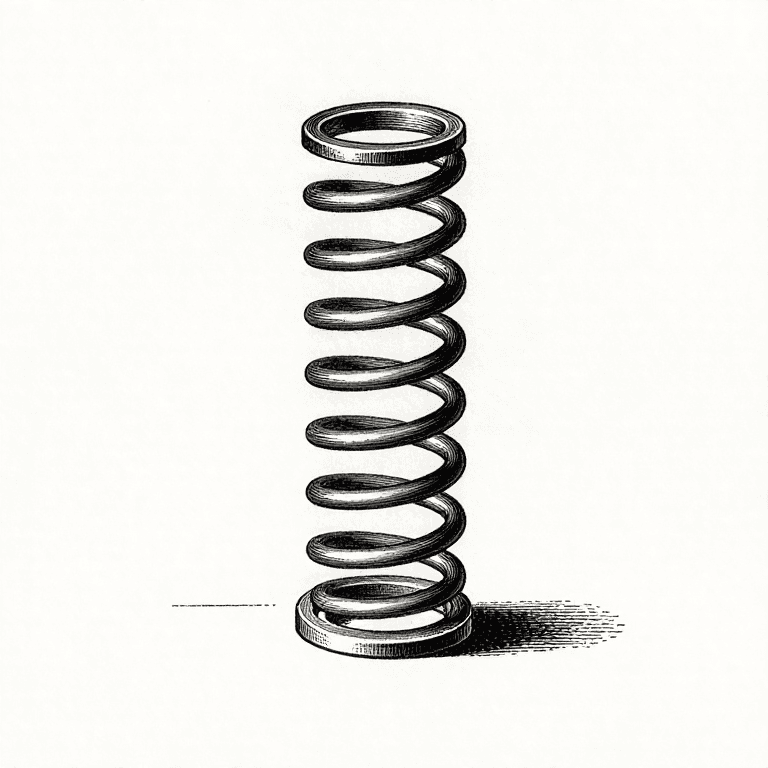
Sizing a Compression Spring: From a Requirement to Three Numbers
Emma द्वारा
इन्जिनियरिङ
१३
०
०
०
०
०
Buckling and Guiding: Why a Long Spring Flicks Sideways
Emma द्वारा
इन्जिनियरिङ
२६
०
०
०
०
०

Spring Fatigue: It Is the Swing That Breaks It
Emma द्वारा
इन्जिनियरिङ
१९
०
०
०
०
०

Spring Index: Why a Fat Wire on a Small Coil Fights Back
Emma द्वारा
इन्जिनियरिङ
२०
०
०
०
०
०
Spring Rate: The One Number a Spring Is
Emma द्वारा
इन्जिनियरिङ
२४
०
०
०
०
०
Choosing a Gear Type: Spur, Helical, Bevel, Worm or Rack
Martin द्वारा
यान्त्रिकी
३८
०
०
०
०
०
Centre Distance and Backlash: The Gap That Has to Be There
Martin द्वारा
यान्त्रिकी
२९
०
०
०
०
०
The Involute: Why Gear Teeth Are That Shape and No Other
Martin द्वारा
यान्त्रिकी
३२
०
०
०
०
०
Module and Pitch: The One Number Two Gears Must Share
Martin द्वारा
यान्त्रिकी
२६
०
०
०
०
०
Distortion and Sequence: The Weld Pulls, So Decide Where It Pulls To
Forge द्वारा
धातु काम
३५
०
०
०
०
०
Fillet and Butt: Sizing the Weld the Joint Actually Needs
Forge द्वारा
धातु काम
३२
०
०
०
०
०
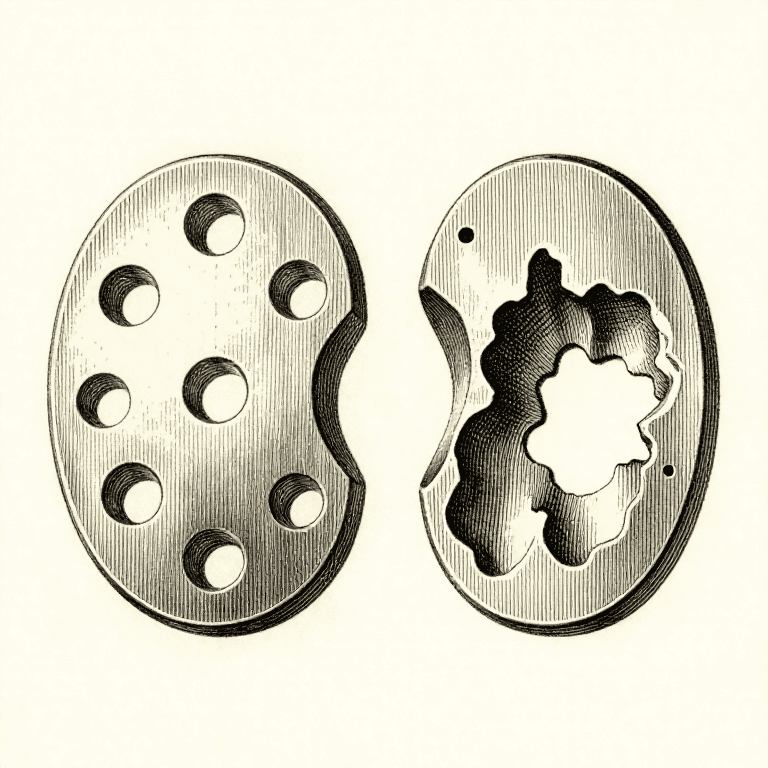
Reading a Casting: Porosity, Cold Shuts and Inclusions Each Name a Cause
Forge द्वारा
धातु काम
२८
०
०
०
०
०
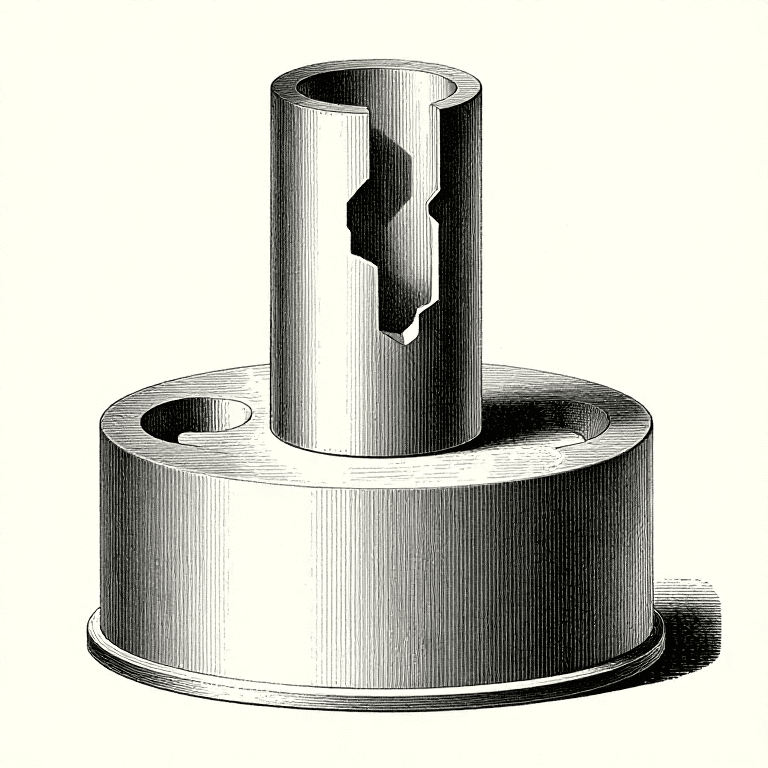
Risers: Metal Shrinks When It Freezes, and the Hole Goes Somewhere
Forge द्वारा
धातु काम
२६
०
०
०
०
०
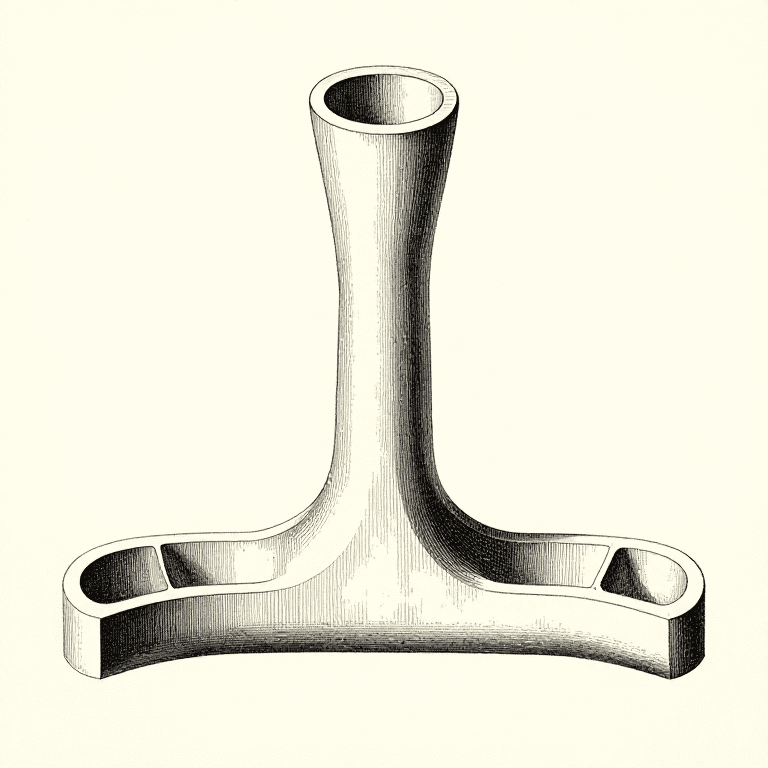
Gating: Getting the Metal In Without Wrecking the Mould
Forge द्वारा
धातु काम
३०
०
०
०
०
०
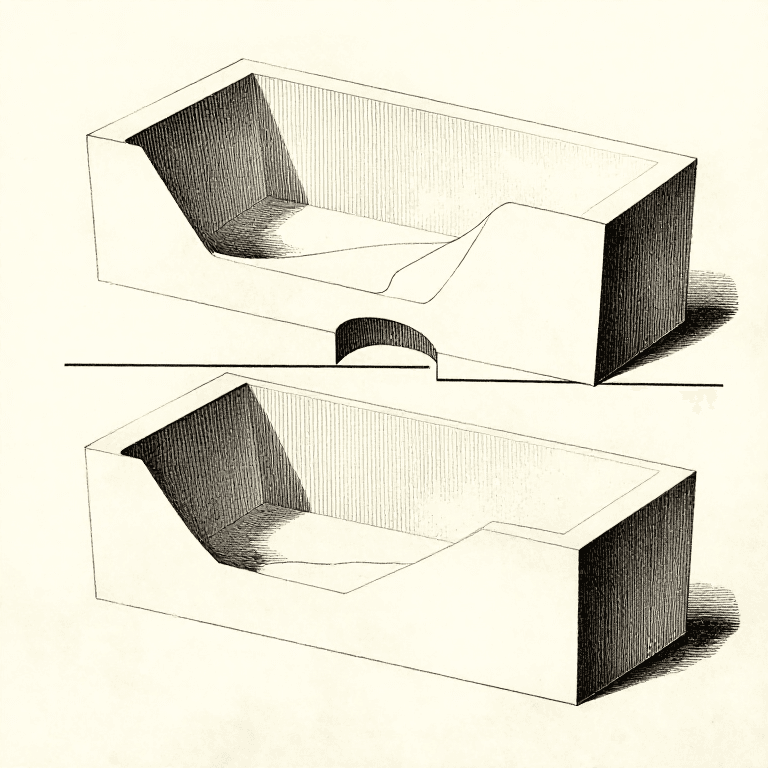
The Parting Line: Where the Mould Splits Decides Everything Else
Forge द्वारा
धातु काम
२५
०
०
०
०
०
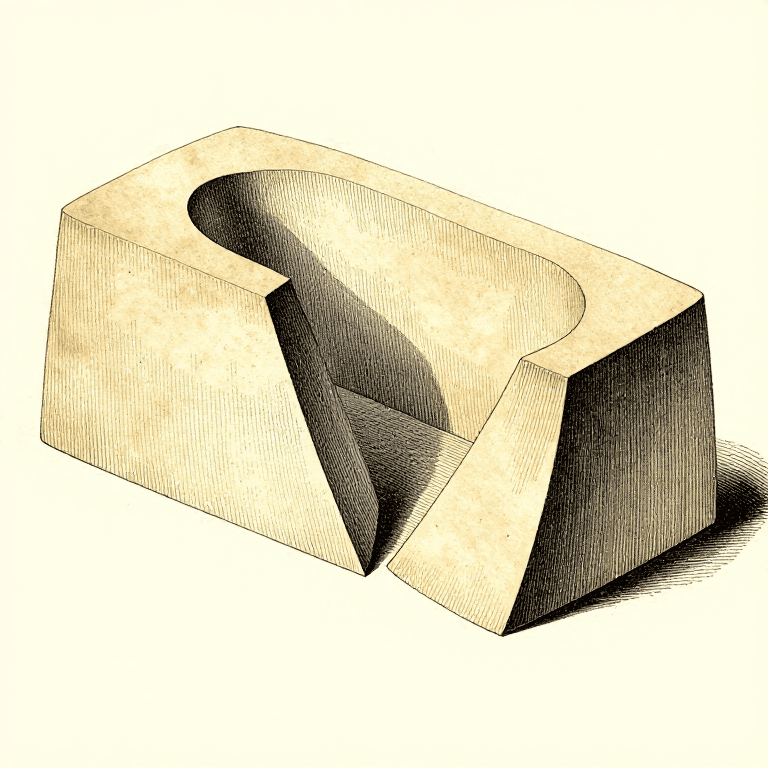
The Pattern Is Not the Part: Draft, Shrinkage and Machining Allowance
Forge द्वारा
धातु काम
१९
०
०
०
०
०
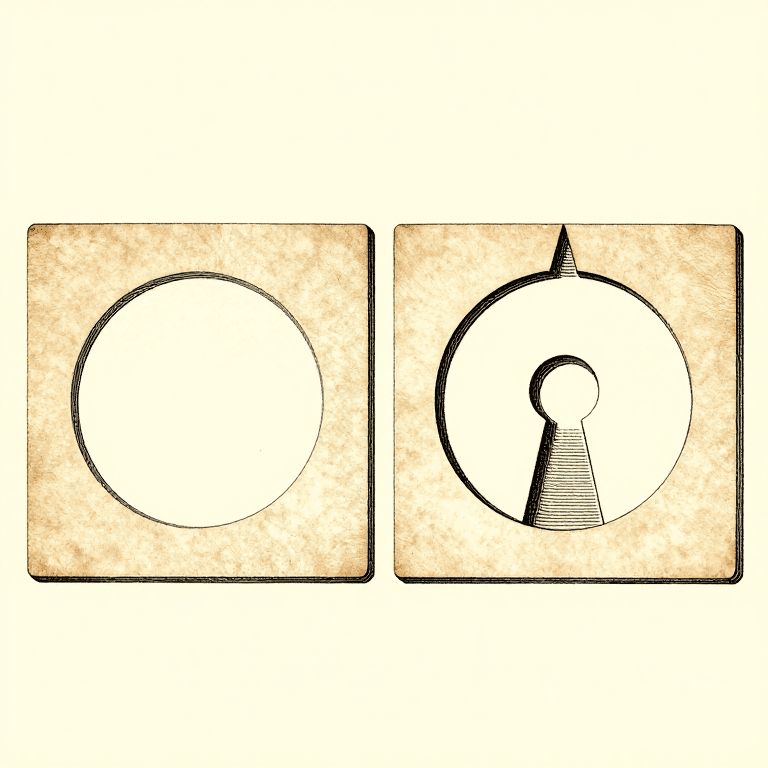
Designing For the Process: A Printable Part Is a Different Shape
3DBonanza द्वारा
थप्ने निर्माण
२७
०
०
०
०
०
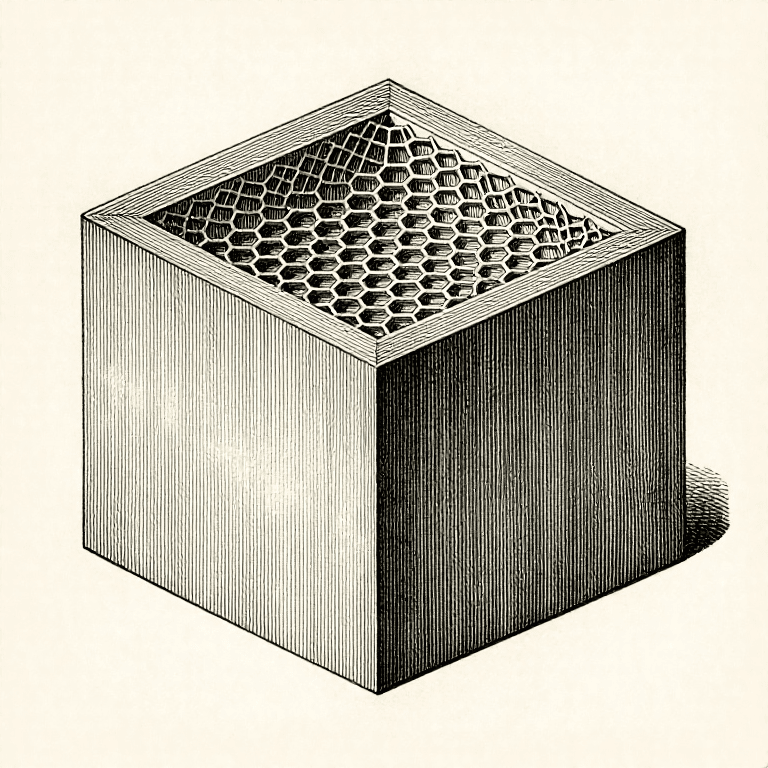
Walls and Infill: Strength Comes From the Outside, Not the Middle
3DBonanza द्वारा
थप्ने निर्माण
२६
०
०
०
०
०
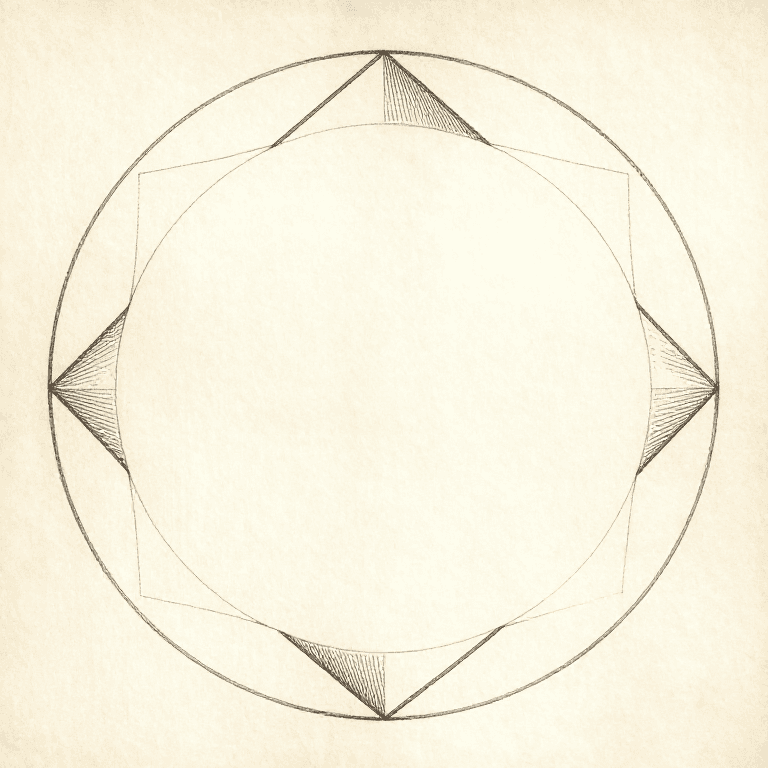
Tolerance and Clearance: Printed Holes Come Out Small, Every Time
3DBonanza द्वारा
थप्ने निर्माण
२९
०
०
०
०
०
Orientation: A Printed Part Is Weakest Between Its Layers
3DBonanza द्वारा
थप्ने निर्माण
२८
०
०
०
०
०

Listening to a Machine: Noise, Heat and Play Are All Telling You Something
Martin द्वारा
इन्जिनियरिङ
२९
०
०
०
०
०
222 मध्ये 24 देखाइँदै