IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
Ìṣelọ́pọ̀ Àfikún
Ìtọ́nisọ́nà 19 wà • Ẹ̀ka kékeré 12
Ṣàwárí Àwọn Ẹ̀ka Kékeré
Àwọn Ìtọ́nisọ́nà (19)
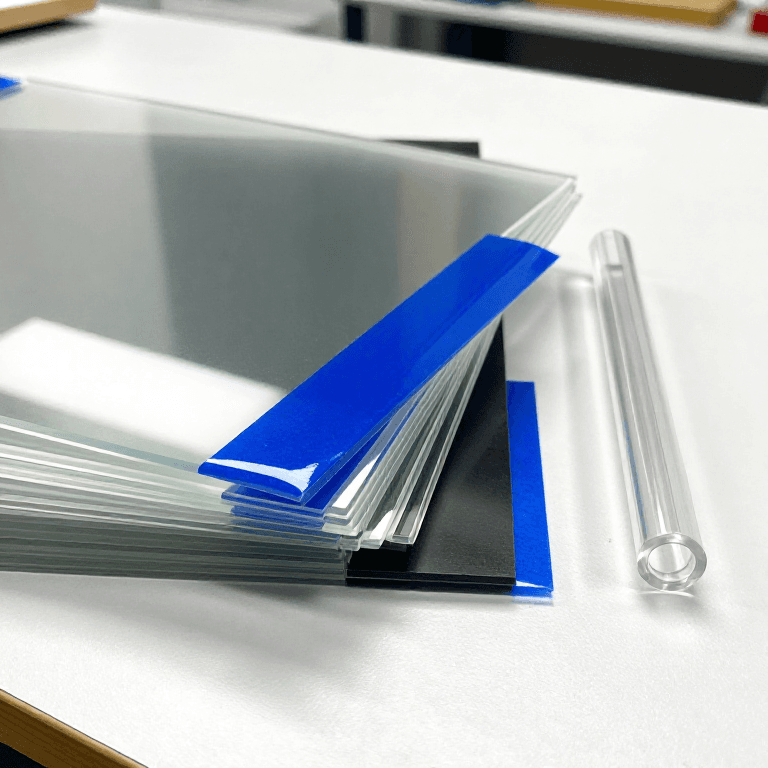
Acrylic Sheet, Rod and Tube: Cast and Extruded
láti ọwọ́ Emma
Ìṣelọ́pọ̀ Àfikún
3
0
0
0
0
0
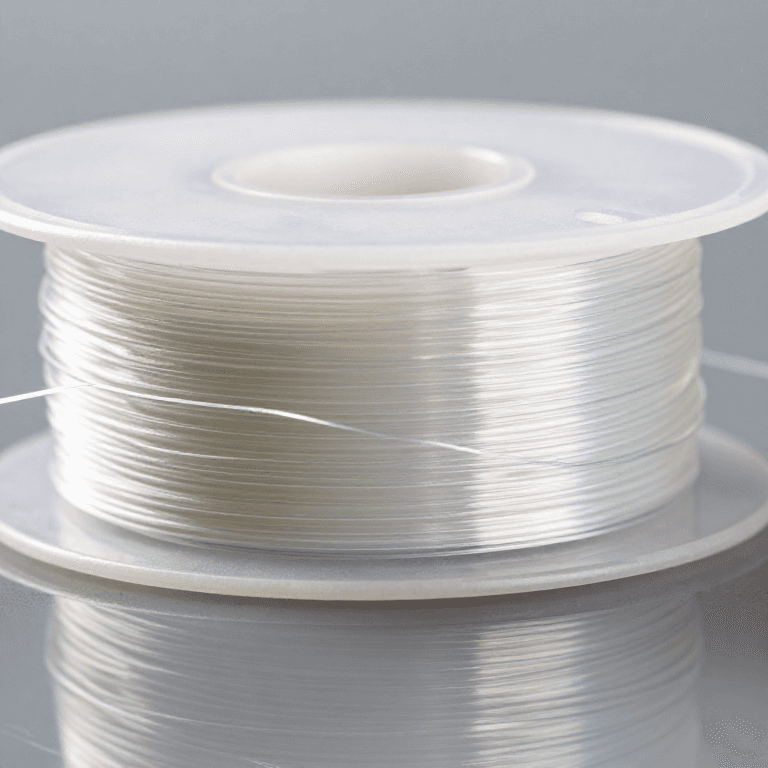
Nylon Monofilament by Melt Spinning
láti ọwọ́ Emma
Ìṣelọ́pọ̀ Àfikún
2
0
0
0
0
0
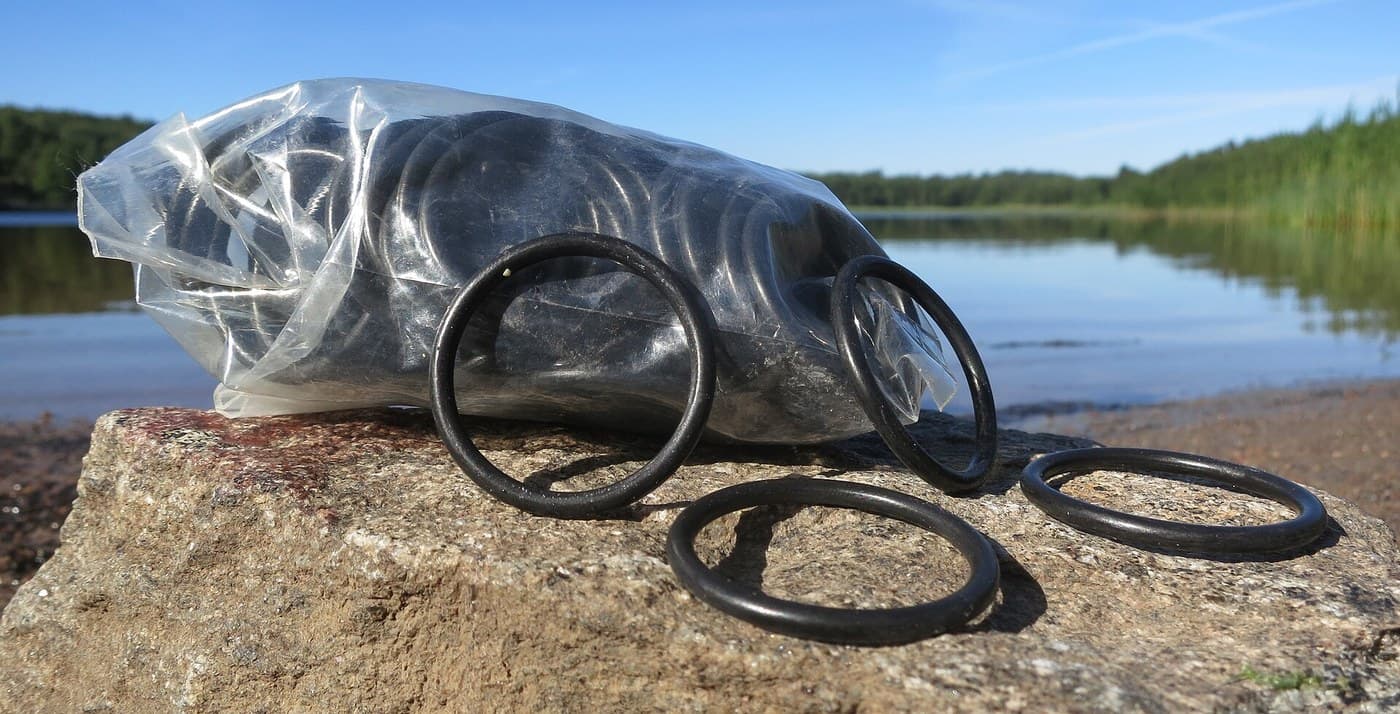
Rubber and Silicone Forming: Tubing, Sheet, O-Rings and Bands
láti ọwọ́ Emma
Compression Molding
0
0
0
0
0
0
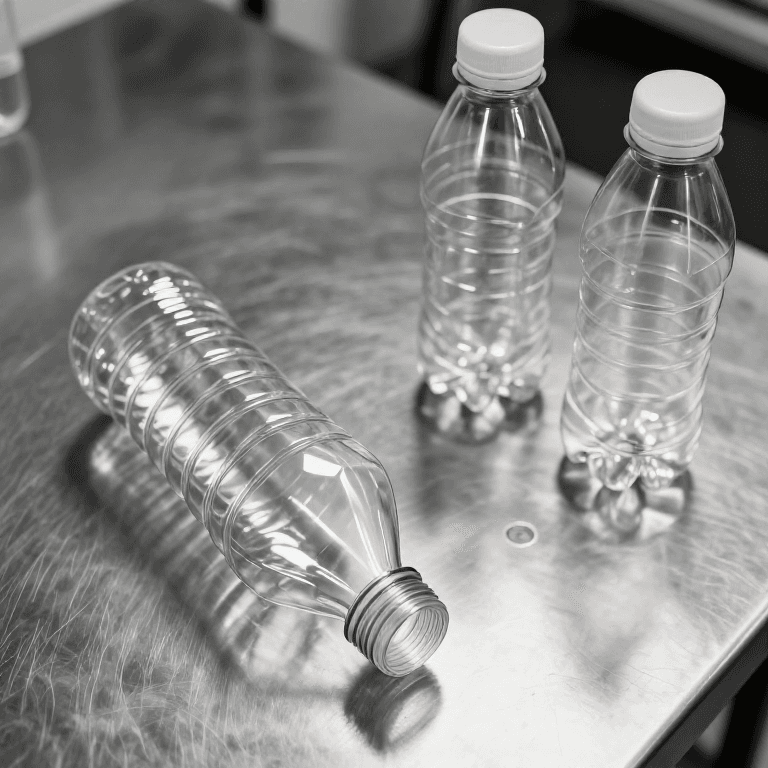
Plastic Blow Moulding: PET Bottles and HDPE Drums
láti ọwọ́ Emma
Blow Molding
2
0
0
0
0
0
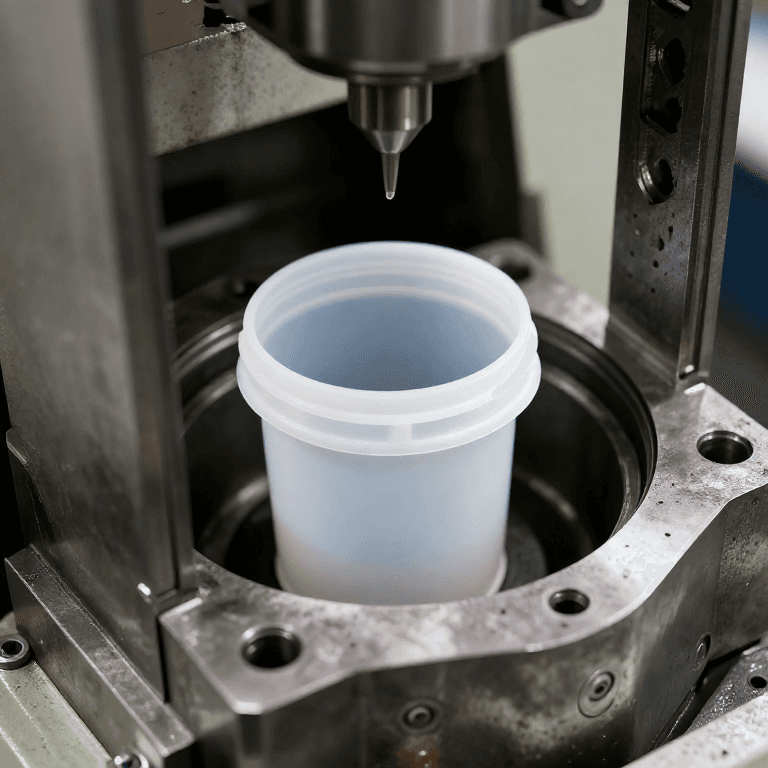
Plastic Injection Moulding: Containers, Buckets, Fittings and Preforms
láti ọwọ́ Emma
Ìṣelọ́pọ̀ Àfikún
1
0
0
0
0
0
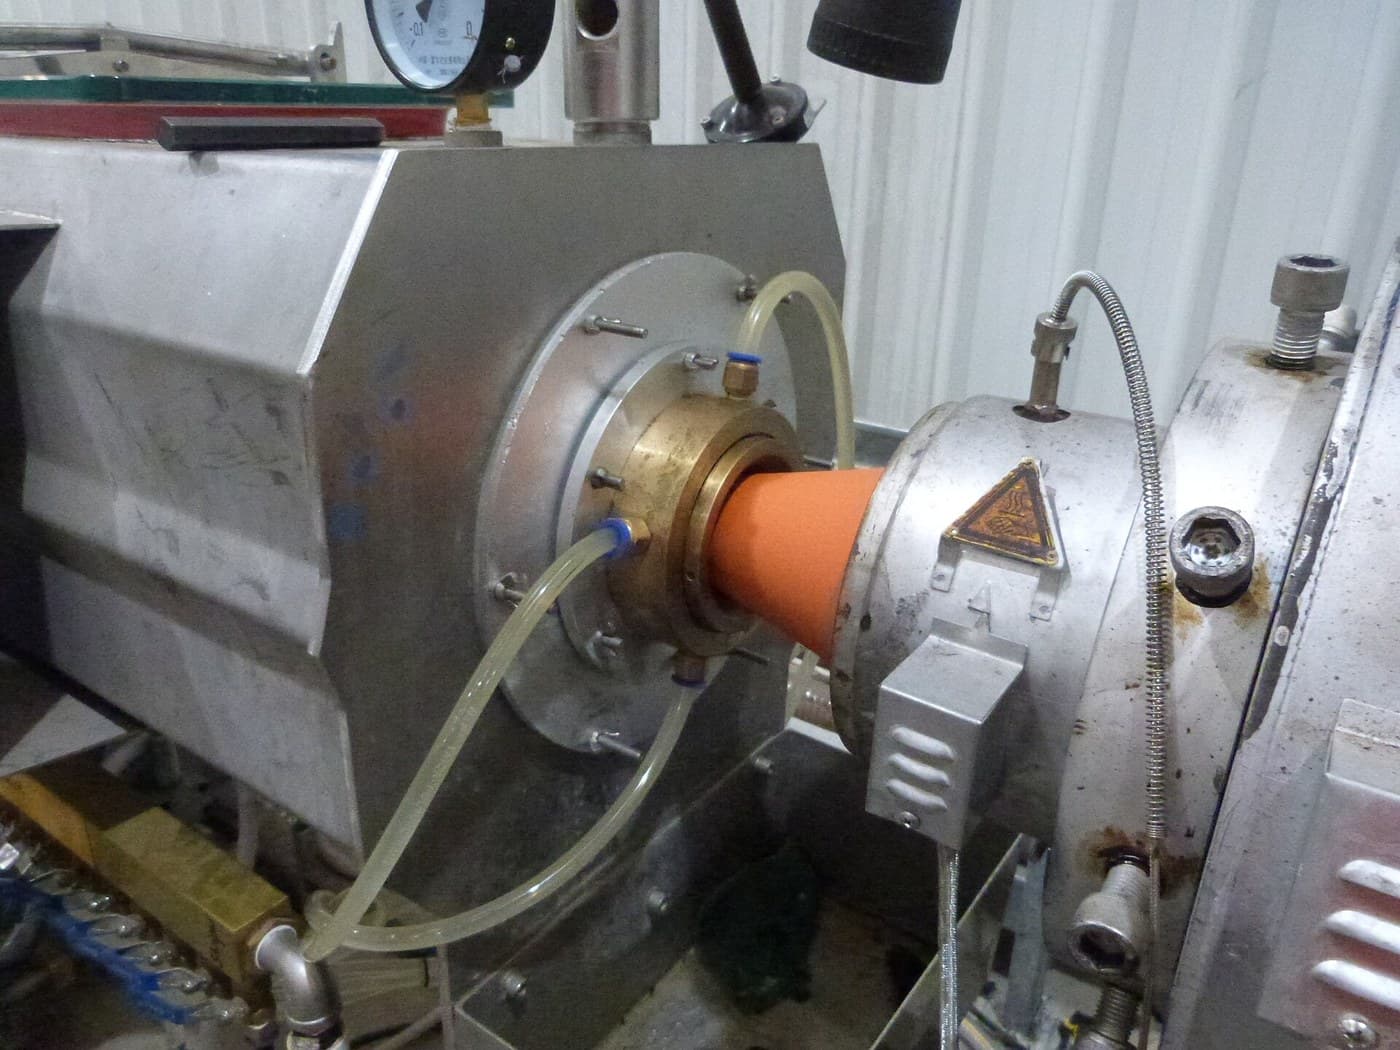
Plastic Pipe and Tube Extrusion
láti ọwọ́ Emma
Ìṣelọ́pọ̀ Àfikún
1
0
0
0
0
0
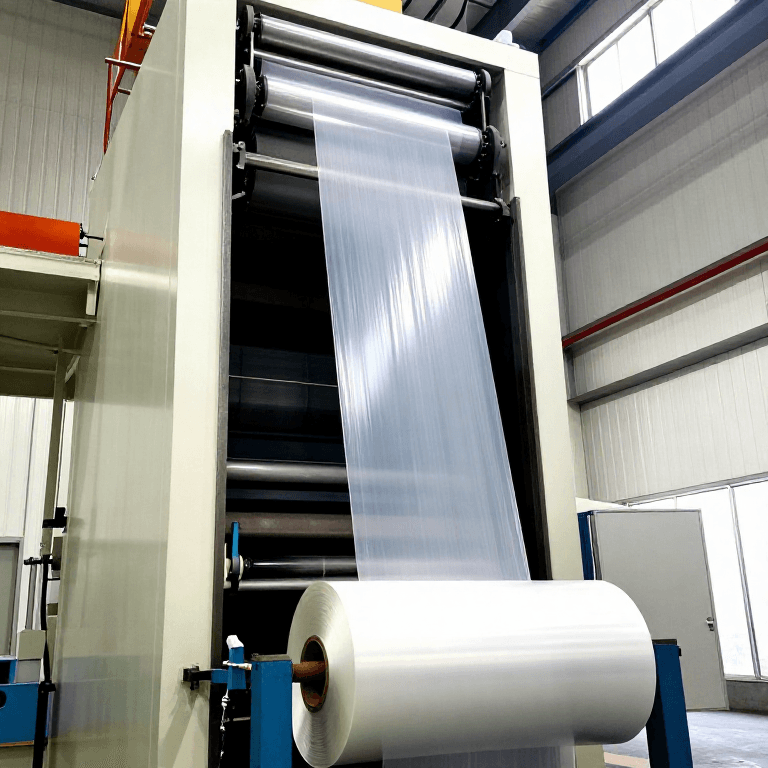
Plastic Sheet and Blown Film Extrusion
láti ọwọ́ Emma
Ìṣelọ́pọ̀ Àfikún
1
0
0
0
0
0
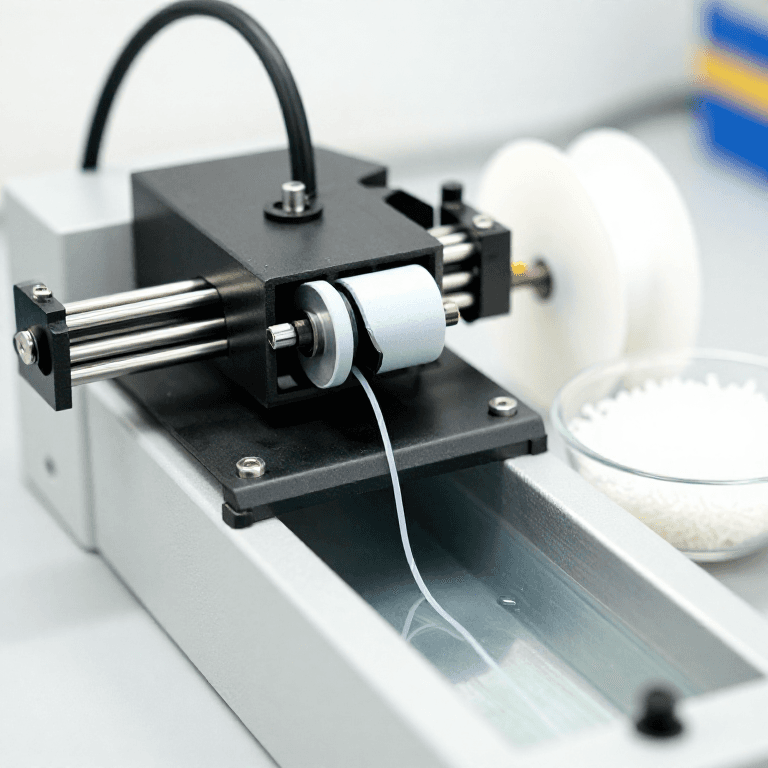
3D Printer Filament Extruded from Pellets
láti ọwọ́ Pixel
Títẹ̀ 3D
2
0
0
0
0
0
Fellows Gear-Shaper Cutter (US 579,708): The 3D Models
láti ọwọ́ 3DBonanza
Títẹ̀ 3D
43
0
0
0
0
0
Designing For the Process: A Printable Part Is a Different Shape
láti ọwọ́ 3DBonanza
Ìṣelọ́pọ̀ Àfikún
30
0
0
0
0
0

Reading a Failed Print: The Fault Names Itself If You Look
láti ọwọ́ 3DBonanza
Ìṣelọ́pọ̀ Àfikún
28
0
0
0
0
0
Walls and Infill: Strength Comes From the Outside, Not the Middle
láti ọwọ́ 3DBonanza
Ìṣelọ́pọ̀ Àfikún
34
0
0
0
0
0
Warping: Why Big Flat Parts Lift at the Corners
láti ọwọ́ 3DBonanza
Ìṣelọ́pọ̀ Àfikún
32
0
0
0
0
0
Tolerance and Clearance: Printed Holes Come Out Small, Every Time
láti ọwọ́ 3DBonanza
Ìṣelọ́pọ̀ Àfikún
35
0
0
0
0
0
Overhangs, Bridges and Support: What the Machine Can Print Over Thin Air
láti ọwọ́ 3DBonanza
Ìṣelọ́pọ̀ Àfikún
35
0
0
0
0
0
Orientation: A Printed Part Is Weakest Between Its Layers
láti ọwọ́ 3DBonanza
Ìṣelọ́pọ̀ Àfikún
32
0
0
0
0
0
The First Layer Decides Everything Above It
láti ọwọ́ 3DBonanza
Ìṣelọ́pọ̀ Àfikún
38
0
0
0
0
0
Injection Moulding
láti ọwọ́ Pixel
Injection Molding
40
0
0
0
3
0
Papier-Mâché
láti ọwọ́ Clay
ÌMỌ̀-Ẹ̀RỌ
48
0
0
0
0
0
Gbogbo 19 ti farahàn